Quick Summary
- What affects tube laser cutting cost comes down to material, tube size and wall, cut complexity, quantity, tolerance and follow-on work.
- Setup is shared across a run, so repeat orders usually cost less per part than one-offs.
- Clean CAD files and complete specs remove back-and-forth that slows quotes.
- This post covers factors only. Blueline does not publish prices, so request a quote for your part.
What affects tube laser cutting cost most are the material, the tube size and wall thickness, how many features each part has, and how many parts you order. Each one changes cutting time or setup effort. This guide explains the factors, not prices.
Blueline Industries runs tube laser cutting from its facility in Chino, CA. We want buyers to understand what moves a quote so they can send better information and make smarter design choices.
What affects tube laser cutting cost the most?
Material, wall thickness, cut complexity and quantity usually matter most. Thicker wall takes longer to cut. More holes, slots and notches add cutting time. Larger quantities spread setup over more parts. Material type also changes cost, since stainless and steel are priced and processed differently.
A fabrication cost article from Fabcon says material type, thickness, cut distance, pierce count and assist gas act as primary cost drivers in laser cutting. That article covers laser cutting in general, but the same logic applies to tube.
How do material and wall thickness change the cost?
Material sets the raw cost of the tube and how the laser cuts it. Wall thickness sets how long each cut takes. Thicker wall means slower cutting, so the same design costs more in heavy wall than in thin wall.
Stainless steel and carbon steel also behave differently. The Fabcon article notes that stainless steel needs nitrogen as an assist gas while carbon steel uses lower-cost oxygen. See how Blueline handles both in stainless steel tube processing and steel tube laser cutting.
Tube shape and size
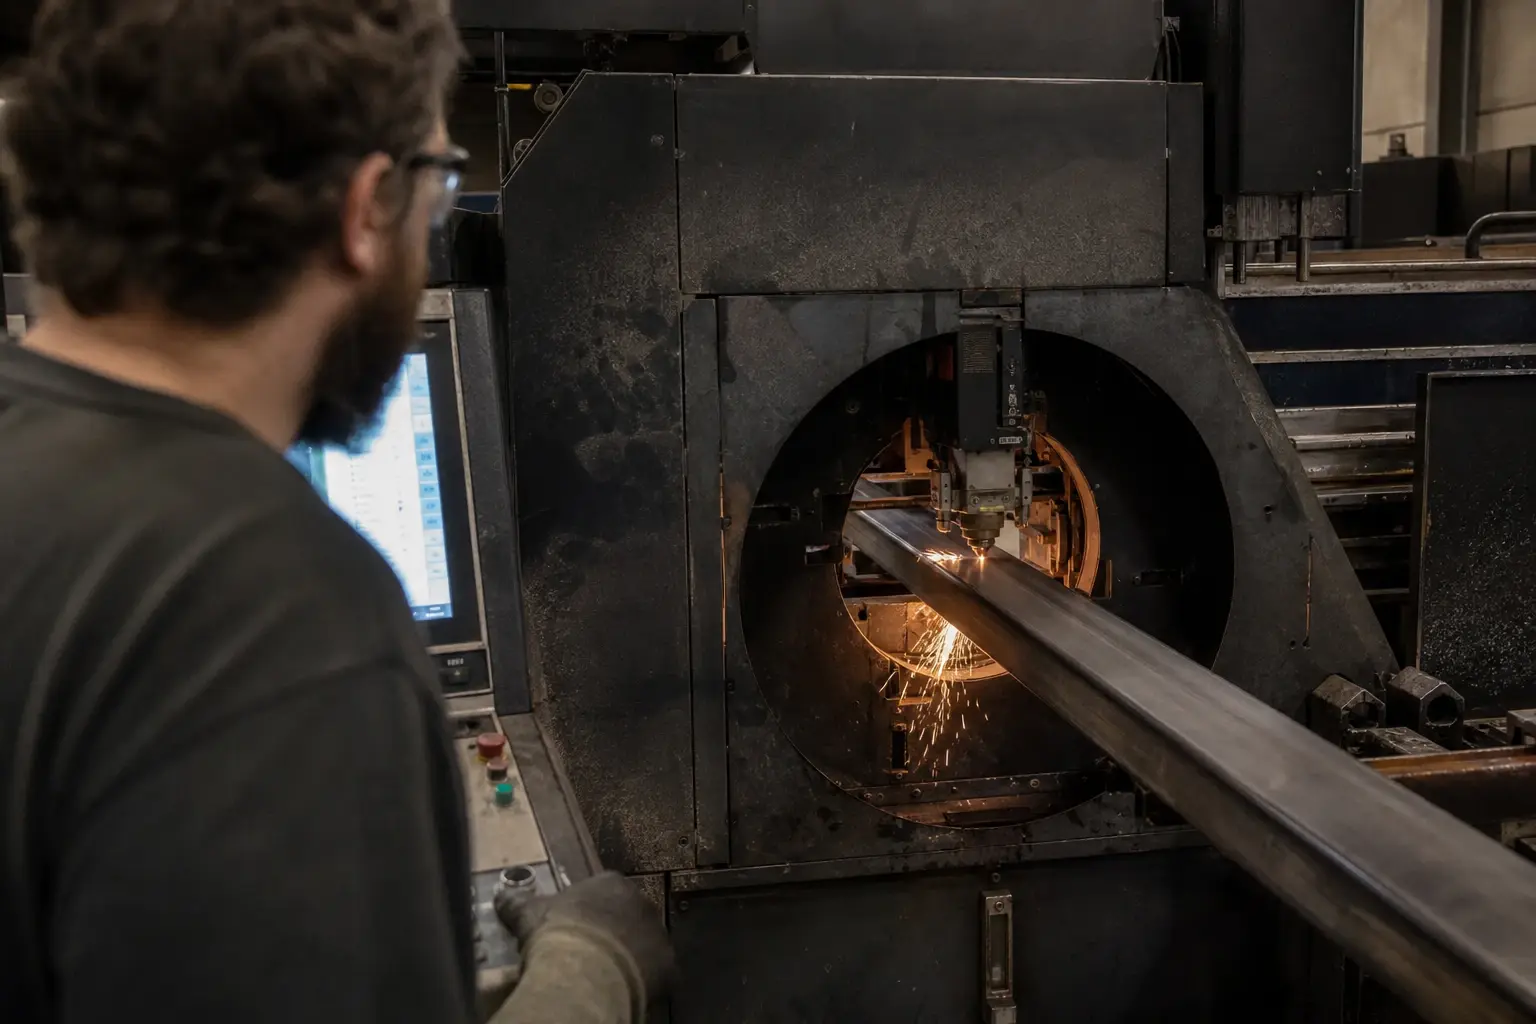
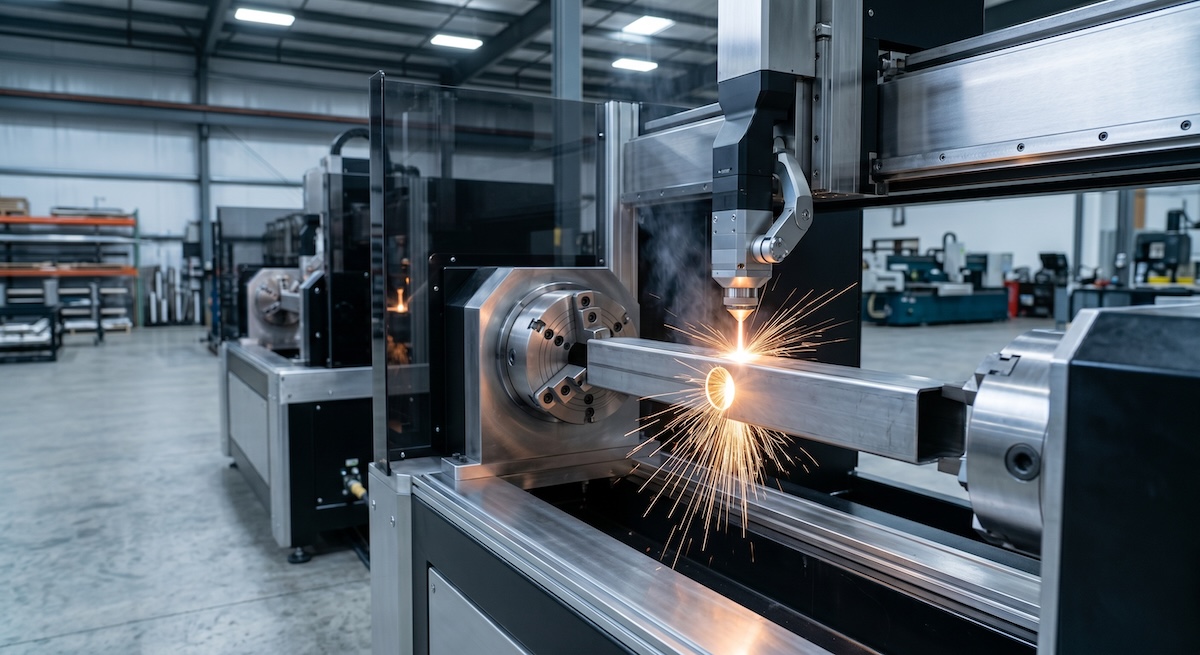
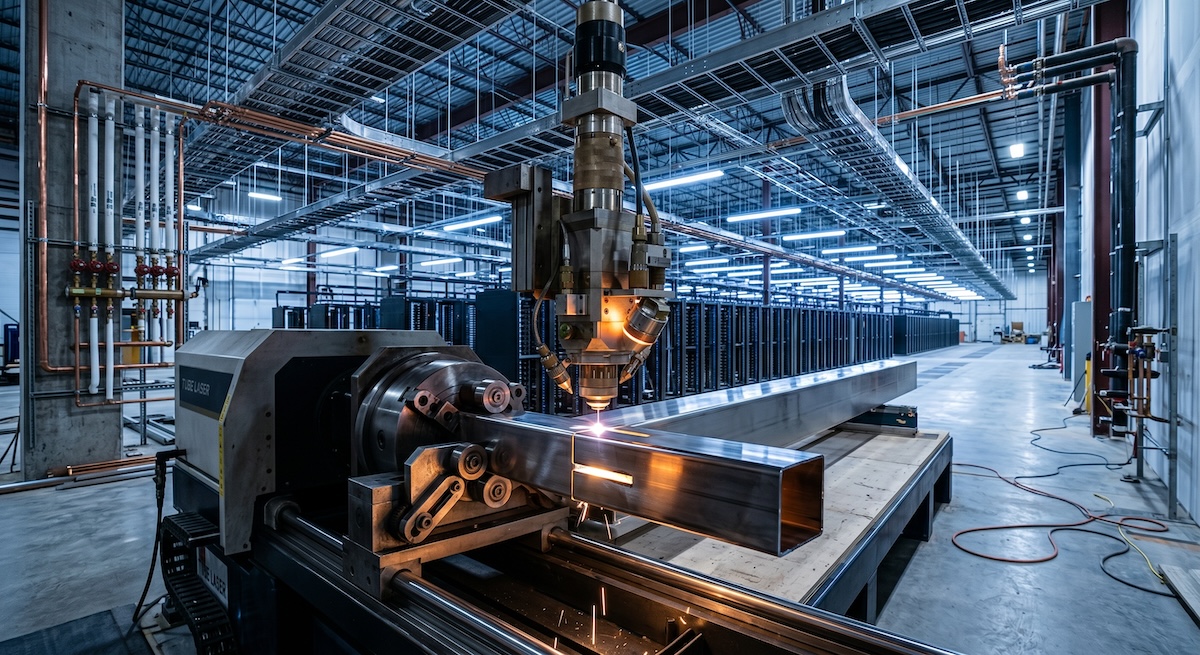
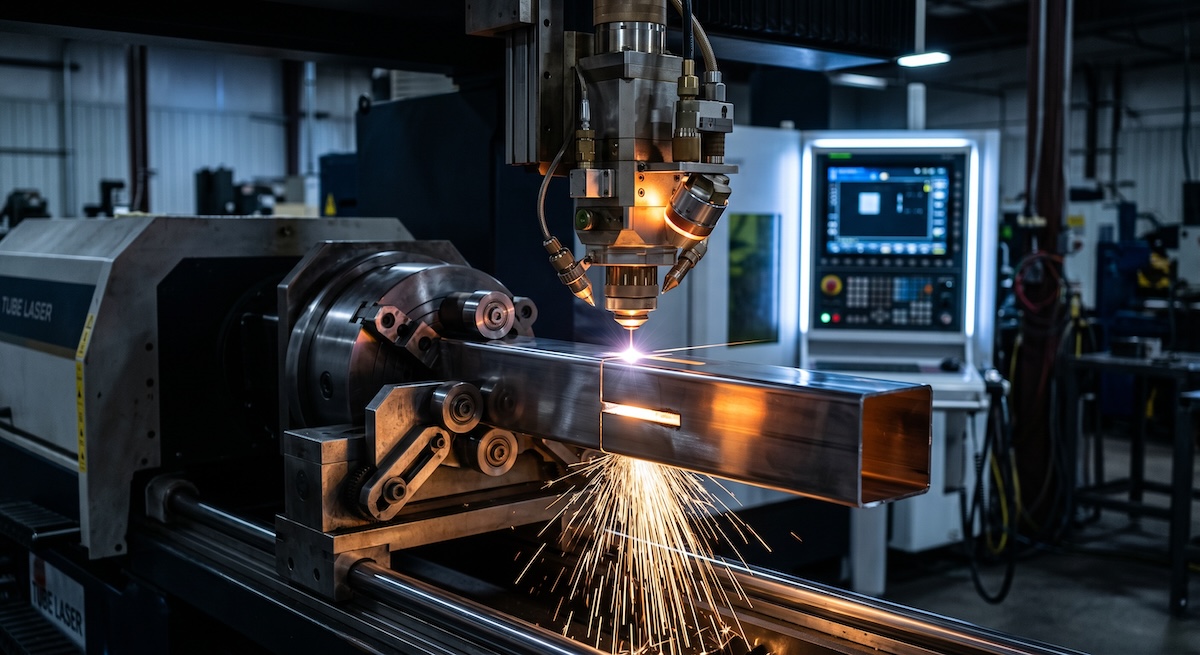
Round, square and rectangular tube each have their own material cost and handling. Larger tube also takes more machine time. Blueline’s LT7 tube lasers handle up to 6 inch square or round tube, and the shop processes tube up to 13 inch diameter.
Does part complexity affect cost?
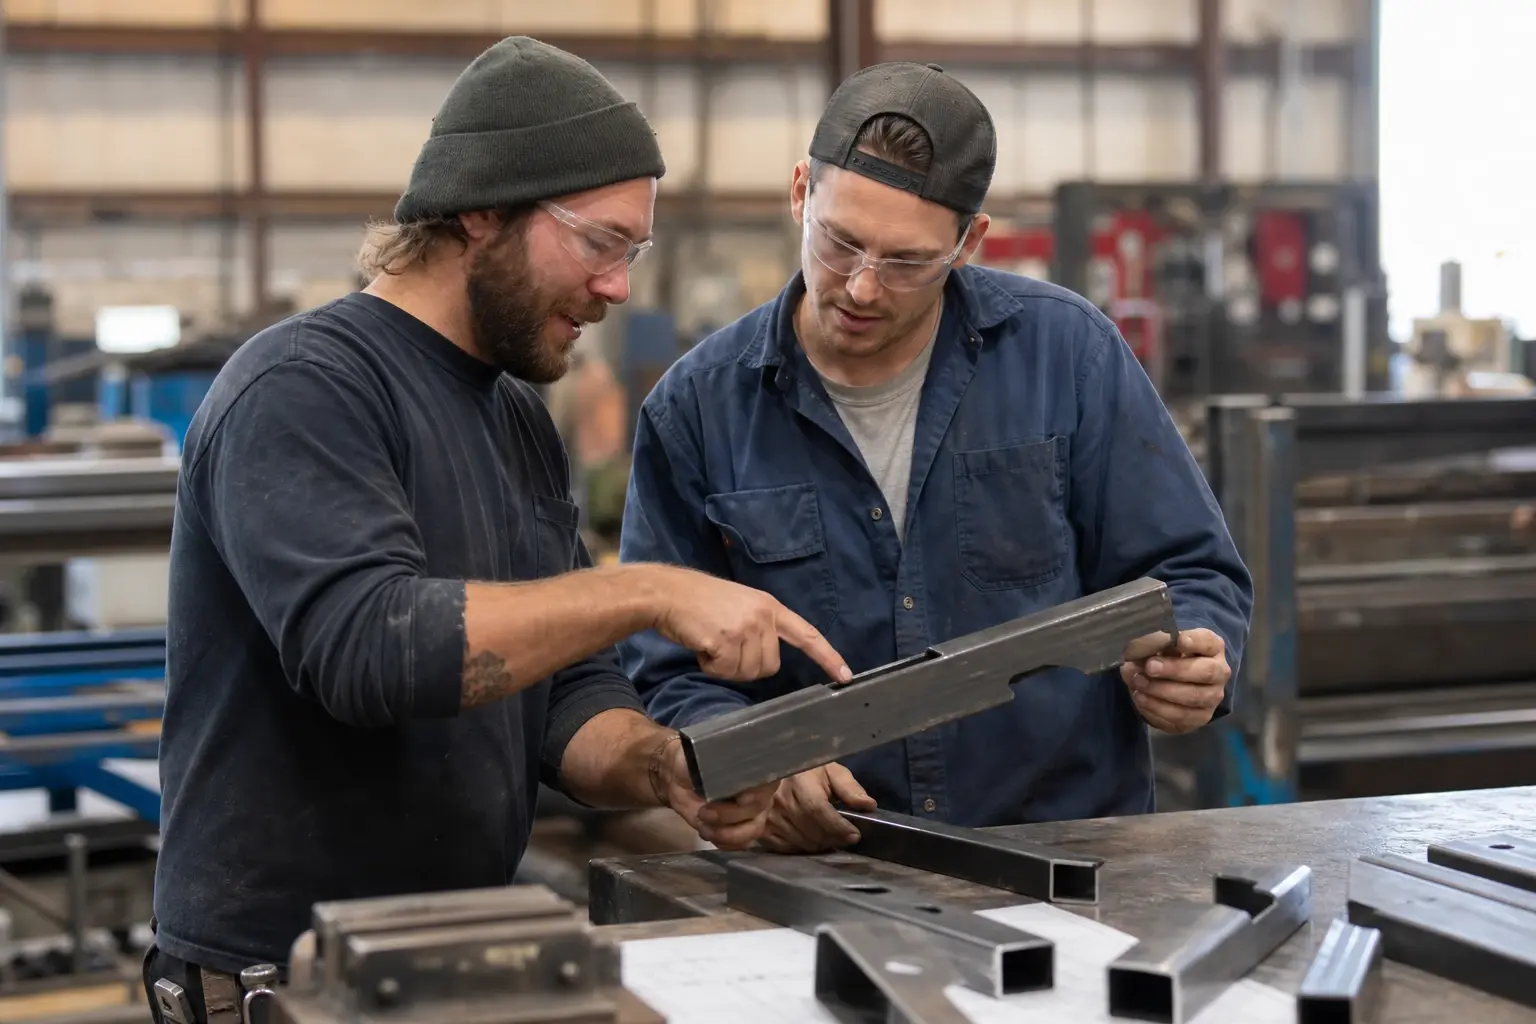
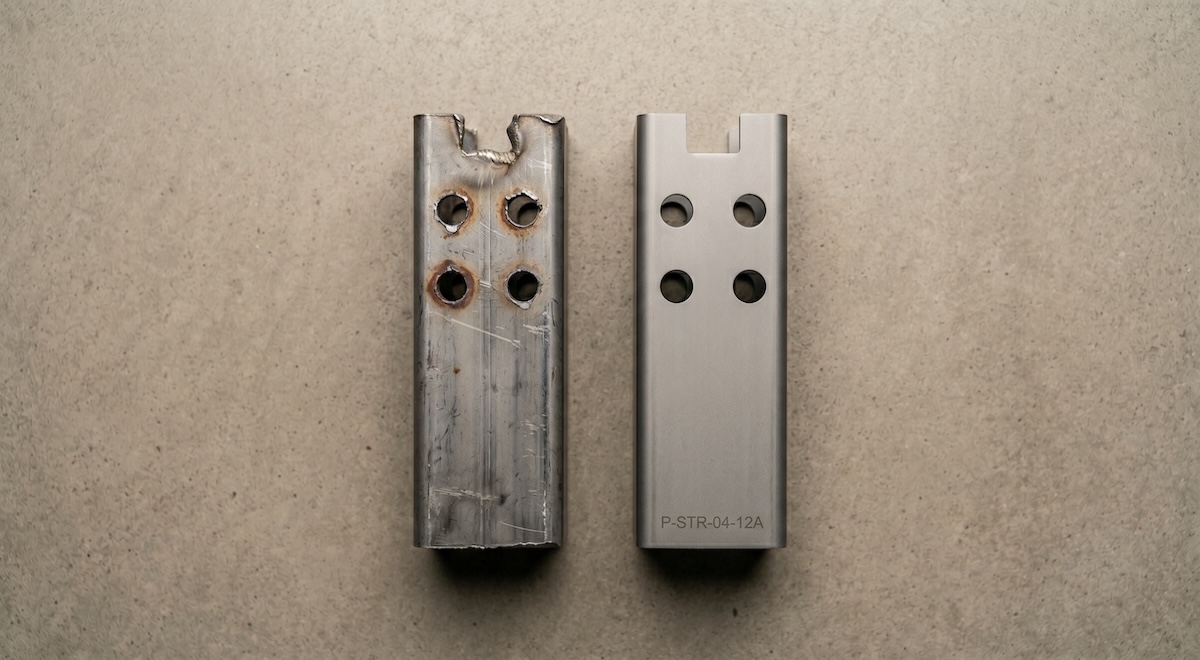
Yes. Every hole, slot and notch adds cutting time, and each point where the laser starts a cut adds to it. A simple cut-to-length part costs less to process than a part with many features. Design only the features the part needs.
Fabcon notes that on thick material, high pierce counts become a major cost driver. Review your drawing for holes and slots that do not serve a function. Our CAD file checklist helps with that review.
Why one price rarely fits every job
Two parts that look alike can cost very different amounts to cut. One may have thin wall and four holes. The other may have heavy wall and forty features. That is why shops quote the part, not the tube. Think of cost as a sum of small decisions made in the design.
How does order quantity change cost per part?
Setup effort is spent once per run, so a larger run spreads it across more parts. A single prototype carries the full setup on one part. A repeat run carries it on many. Per-part cost generally falls as quantity rises.
Fabcon says shops charge a separate setup fee on small one-off jobs to cover operator time, and that setup costs per unit fall at higher quantities. For early designs, prototyping and short-run fabrication lets you prove the design before you scale.
Do tolerances and follow-on work add cost?
They can. Tighter tolerances demand more care and checking. Bending, welding and finishing add steps on top of the cut. Specify tight tolerances only where the fit needs them, and list every follow-on step in your request so the quote is complete.
Blueline states tolerances of plus or minus 0.003 inch and states that single-operation processing reduces error rates by up to 70%. Fewer machine handoffs also means fewer places for the part to be mishandled. Blueline’s press brake bending uses ProBend all-electric press brakes for follow-on forming.
A quick view of the main cost factors
FactorWhat changesWhat you can doMaterialTube cost and cutting methodChoose the grade the application needsWall thicknessCutting time per featureDo not over-specify wallFeatures per partNumber of cuts and startsRemove holes and slots that serve no functionQuantitySetup spread per partCombine orders where it makes senseToleranceChecking and careTighten only fit-critical featuresFollow-on workAdded stepsList bending and finishing up frontTimelineScheduling pressureShare your date early
Design habits that keep cost reasonable
A few habits help on almost every part. Use standard tube sizes where the design allows. Keep wall thickness no heavier than the load needs. Group similar parts so one setup serves several. Tell the shop which features are critical so the rest can be treated with normal care.
How can you get a more accurate quote?
Send complete information the first time. Include the tube spec, a clean CAD file, the quantity, tolerances on fit-critical features and any bending or finishing. Share your needed date as well. A complete request lets the shop price the job without guessing.
- Tube spec: shape, size, wall thickness and material grade.
- CAD file or drawing: with every cut shown.
- Quantity and schedule: one-off, first run or repeat order.
- Tolerance notes: where fit matters most.
- Follow-on work: bending, welding or finishing.
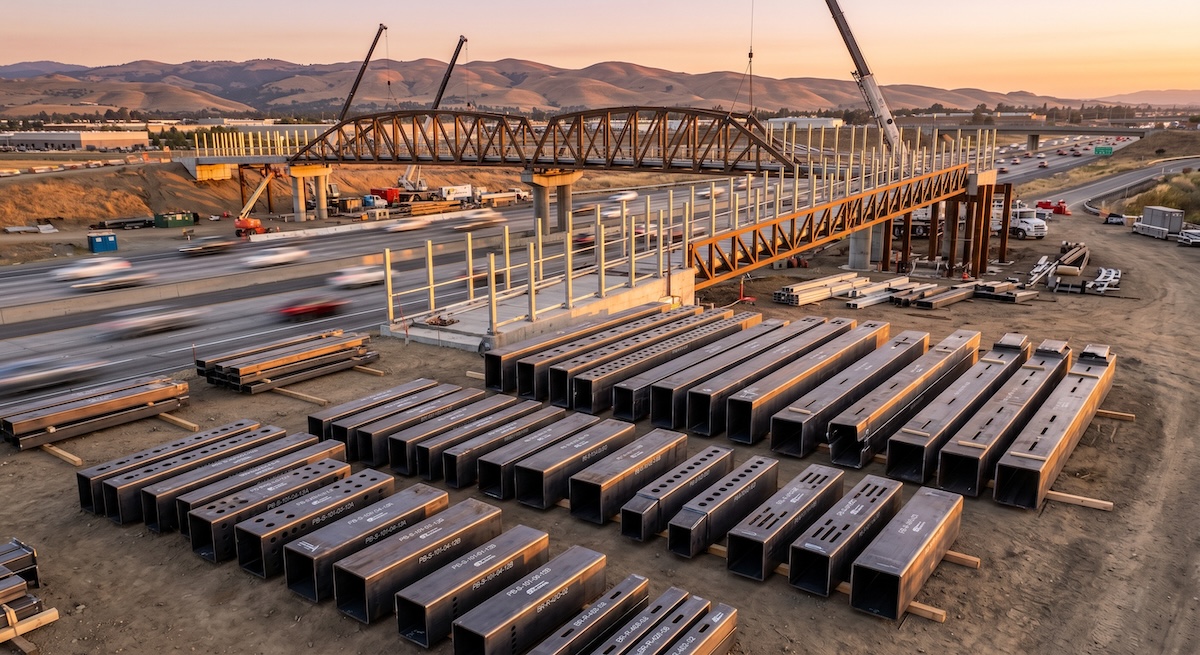
For work that scales, Blueline’s Caltrans I-5 pedestrian bridge project in Irvine involved more than 500,000 pounds of steel in 2025. Big jobs and small jobs follow the same logic: the more complete the information, the more reliable the quote.
Frequently Asked Questions
What is the biggest factor in tube laser cutting cost?
Material, wall thickness, part complexity and quantity usually matter most. Which one leads depends on your part. A simple part in large volume is driven by material, while a complex part in small volume is driven by cutting time and setup.
Does Blueline publish tube laser cutting prices?
No. Pricing depends on the details above, so Blueline quotes each job. Send your spec and CAD file to request a quote.
Does ordering more parts lower the price per part?
Often, yes. Setup is spent once per run, so a larger run spreads it across more parts. A shop will confirm how that applies to your job.
Do complex parts cost more than simple ones?
Generally, yes. More holes, slots and notches mean more cutting time. Removing features that do not serve a function is one of the easiest ways to reduce processing effort.
How fast can I get a quote?
Complete information speeds up the review. Blueline does not promise a set turnaround, but a clear spec and CAD file remove most of the back-and-forth.
Request a Quote for Your Tube Parts
Understanding cost drivers helps you design smarter parts and send better requests. Send your tube spec and CAD file to Blueline in Chino, CA. Get a Quote or call (951) 833-5597.