Quick Summary
- Tube laser cutting for data center supports cuts length, slots, notches and holes from one program, so parts leave the machine ready to fit.
- Tab and slot features let parts locate each other during assembly, which can cut jig setup and measuring before welding.
- Send a dimensioned drawing or 3D model, tube size and wall, material grade, quantity and finish with every quote request.
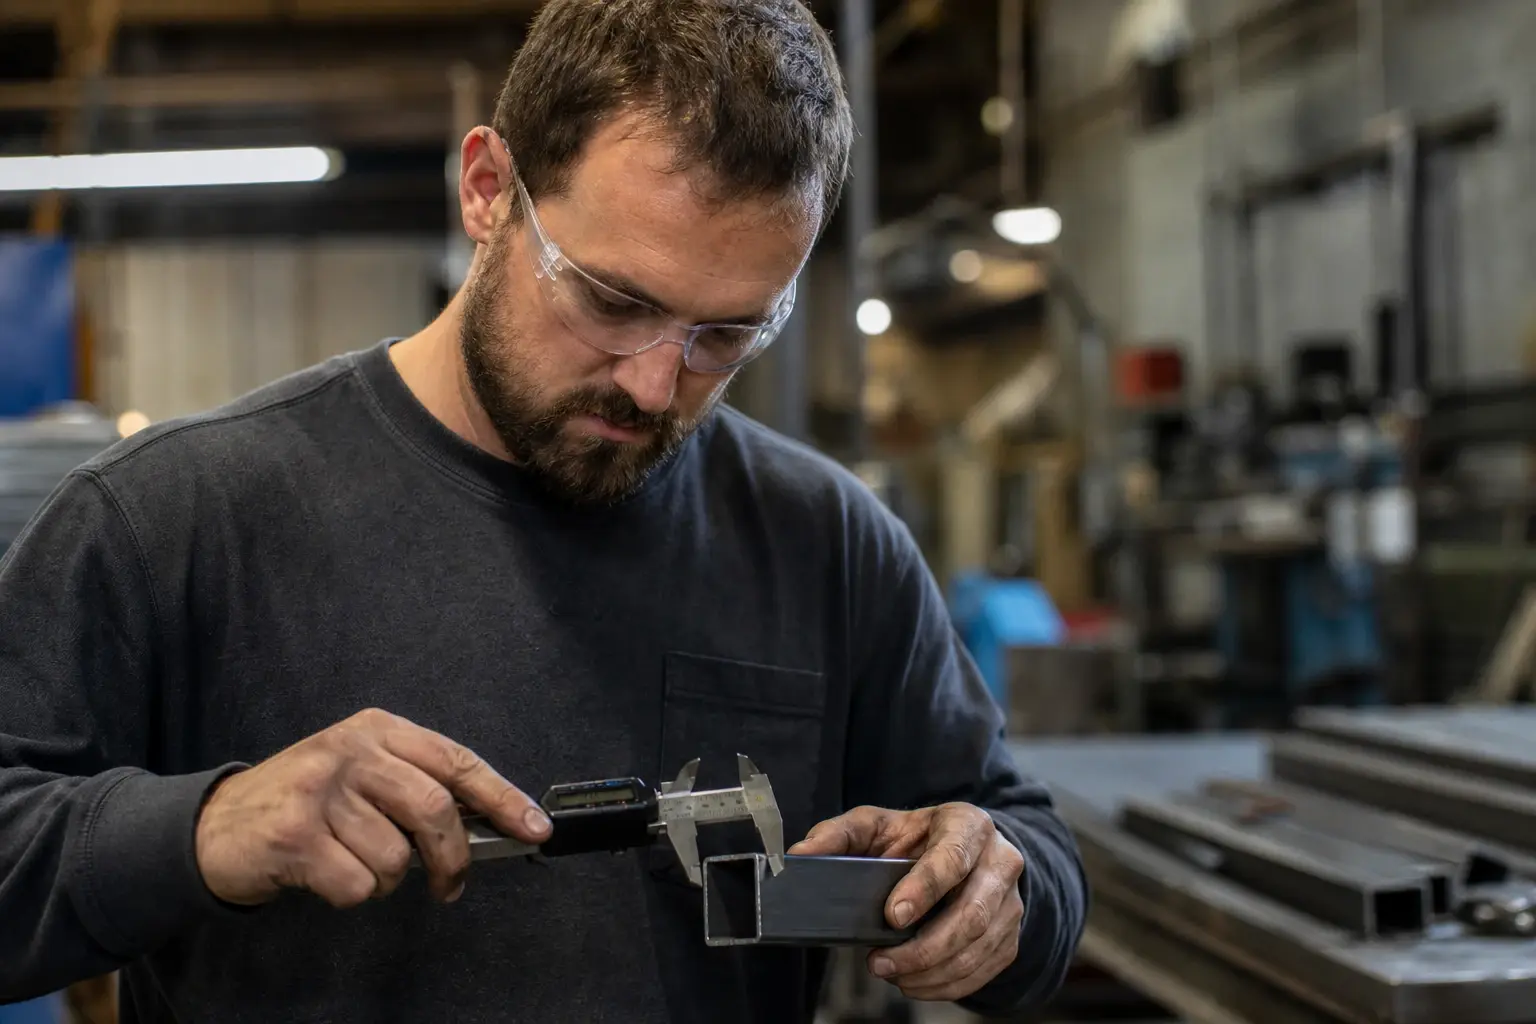
- Blueline states it holds tolerances of plus or minus 0.003 inch from its Chino, CA shop.
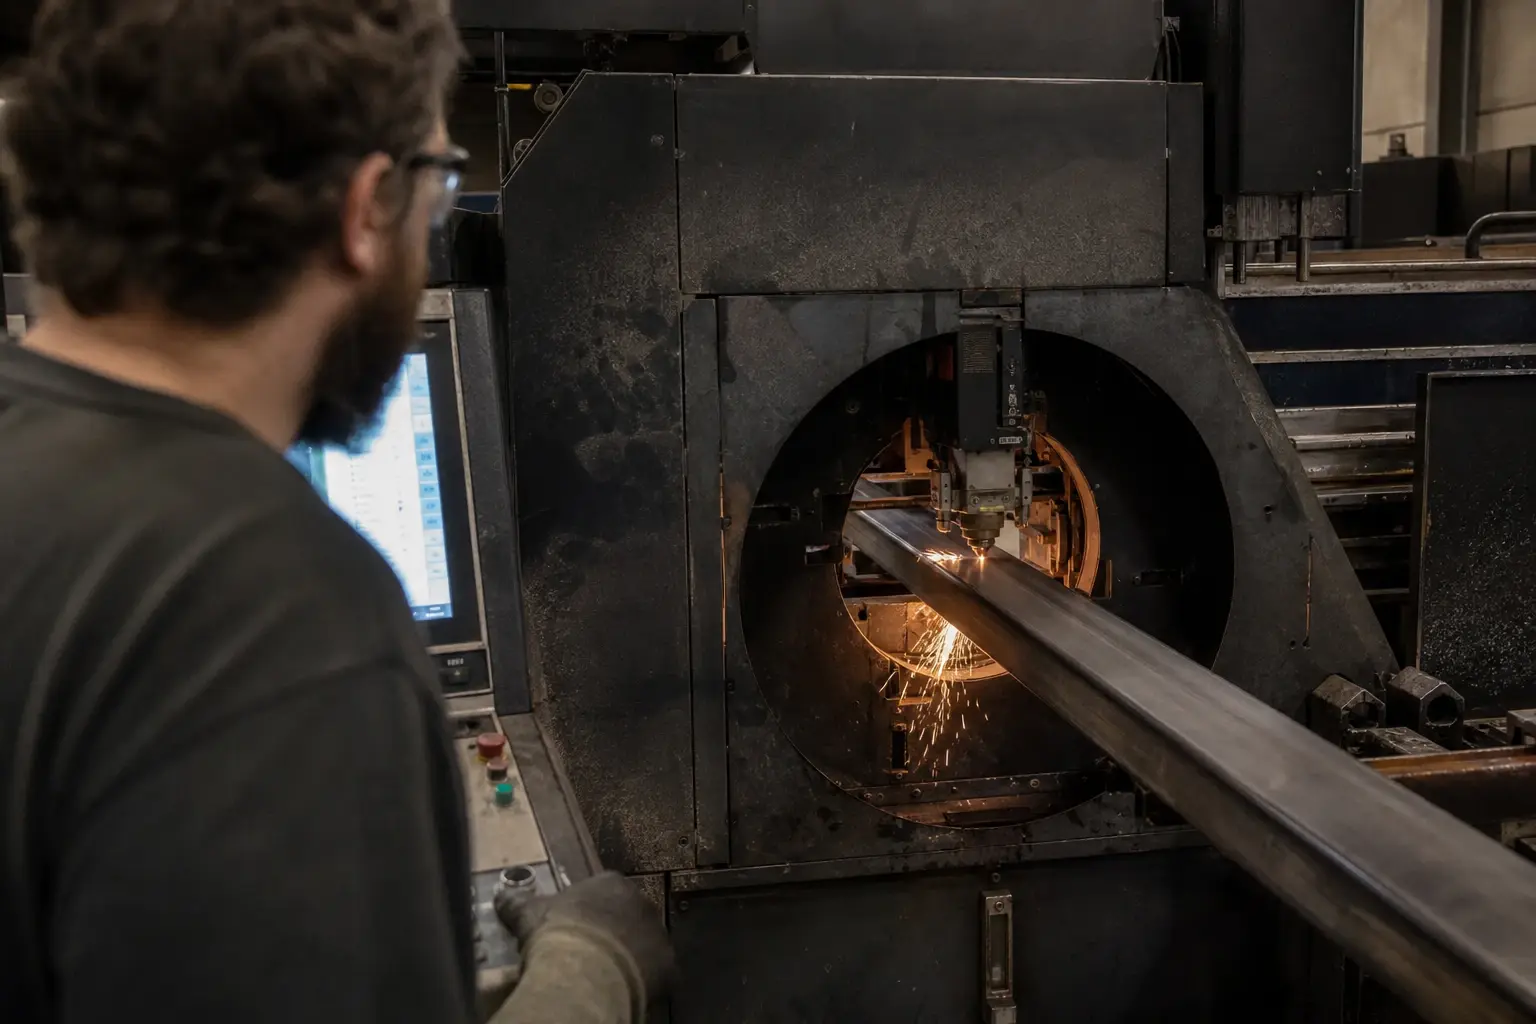
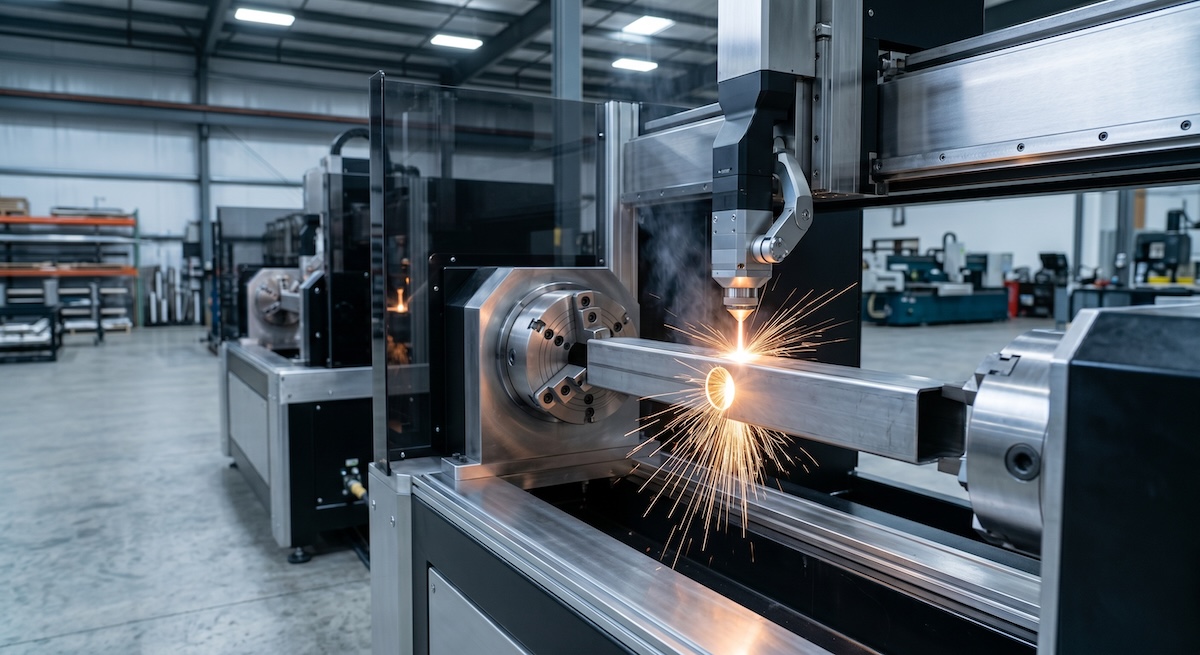
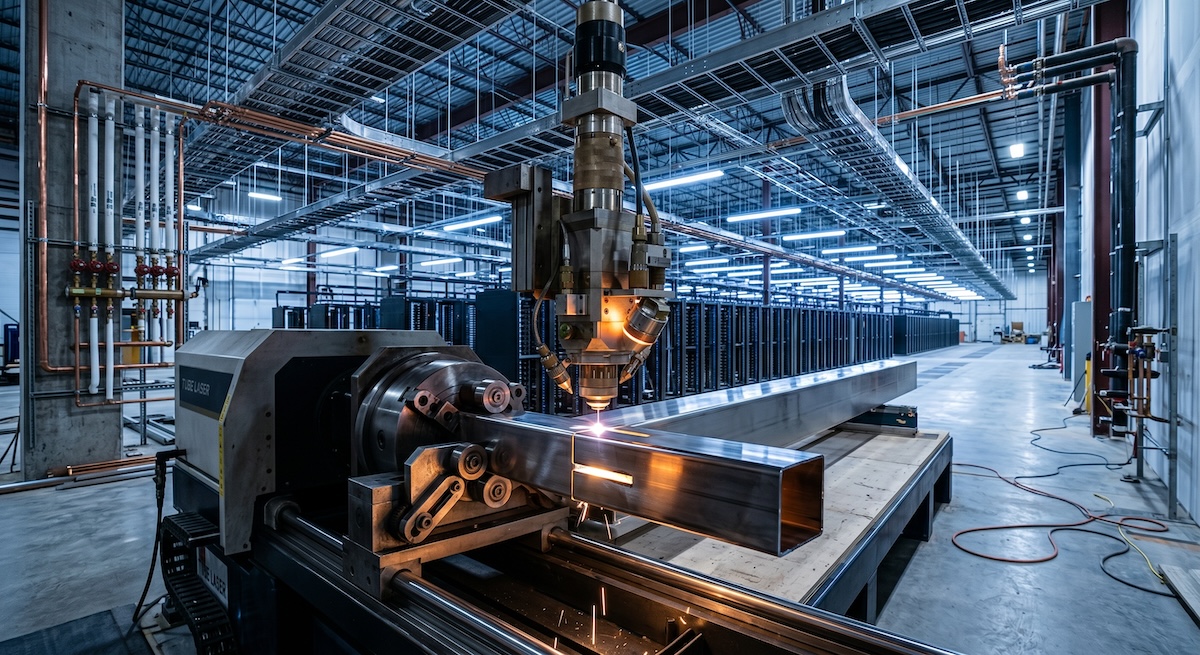
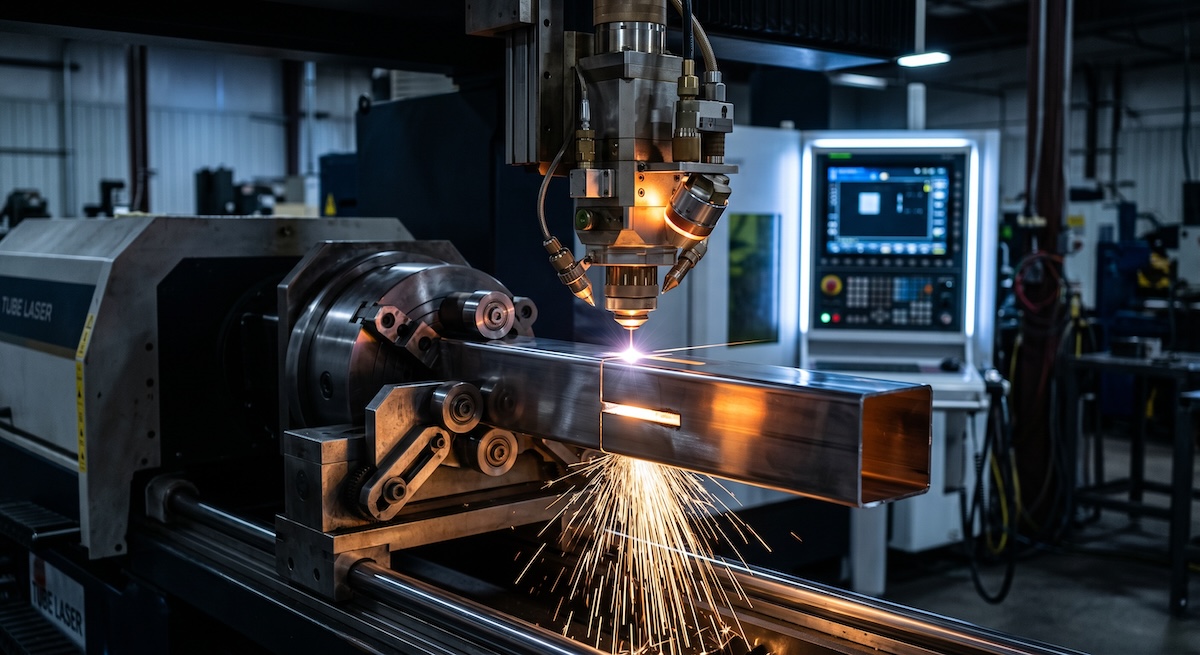
Tube laser cutting for data center supports works best when the parts are designed to be cut, fit and welded with as few separate steps as possible. A tube laser trims a tube to length and adds slots, notches and holes in the same run, so the support reaches the welder ready to assemble.
Blueline Industries runs tube laser cutting from its single facility in Chino, CA. It ships to data center builders in Los Angeles, San Diego, Las Vegas, Salt Lake City, Portland, Seattle and other markets. This post covers what to put on the drawing so your supports come back right the first time.
What counts as a data center support, and why cut it on a tube laser?
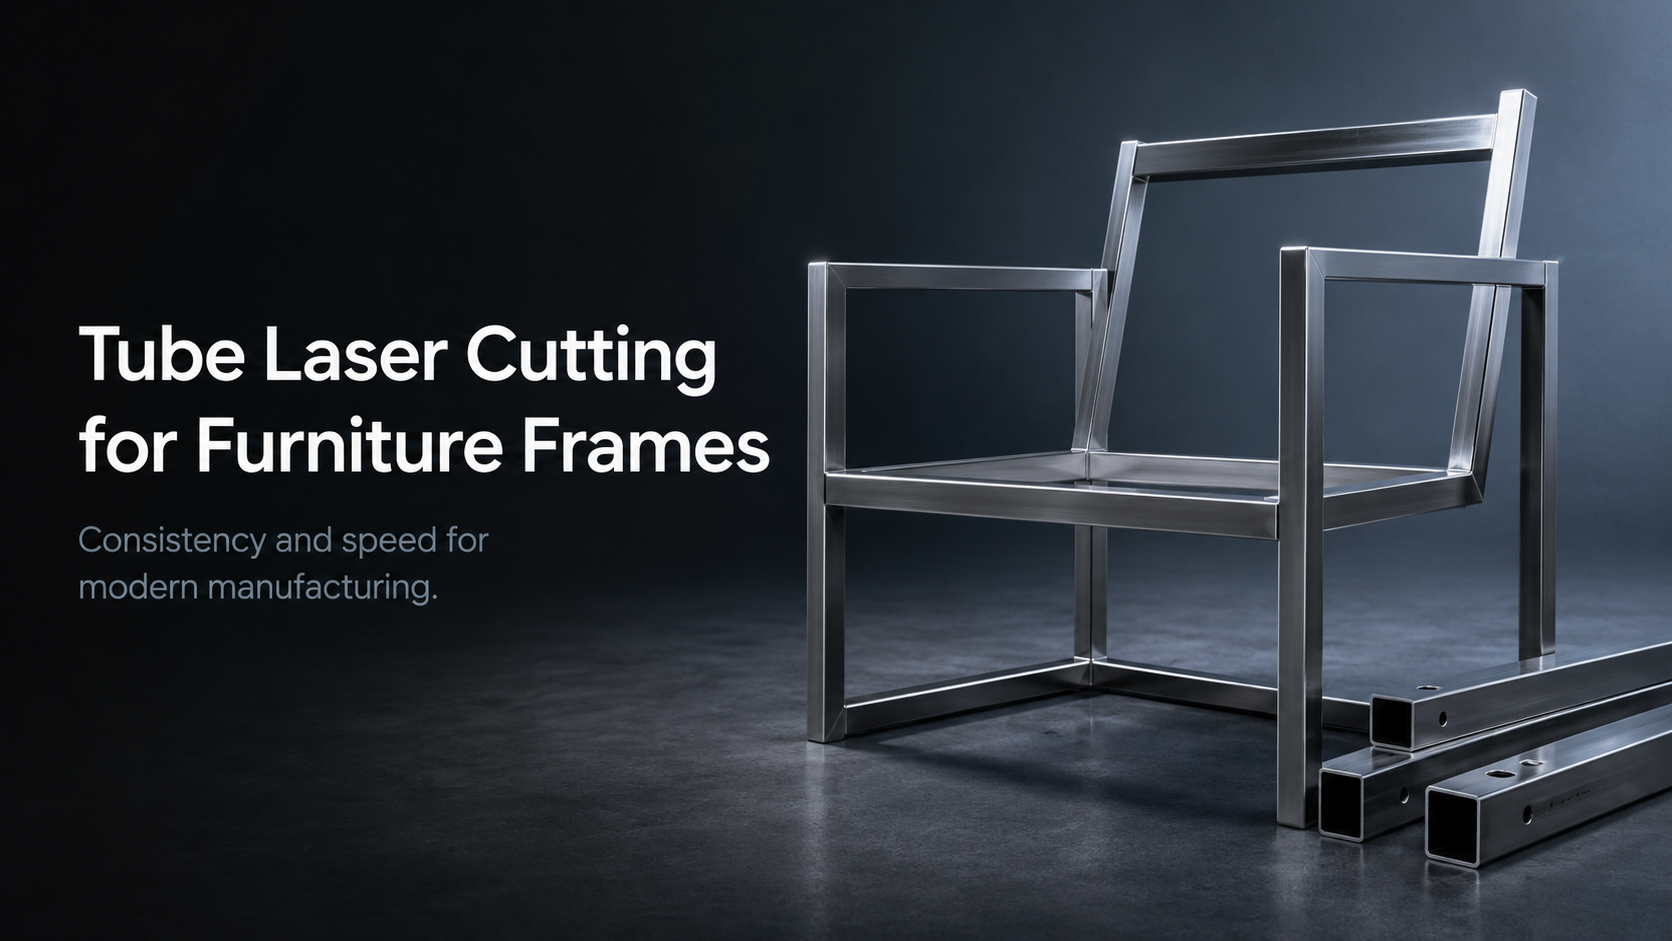
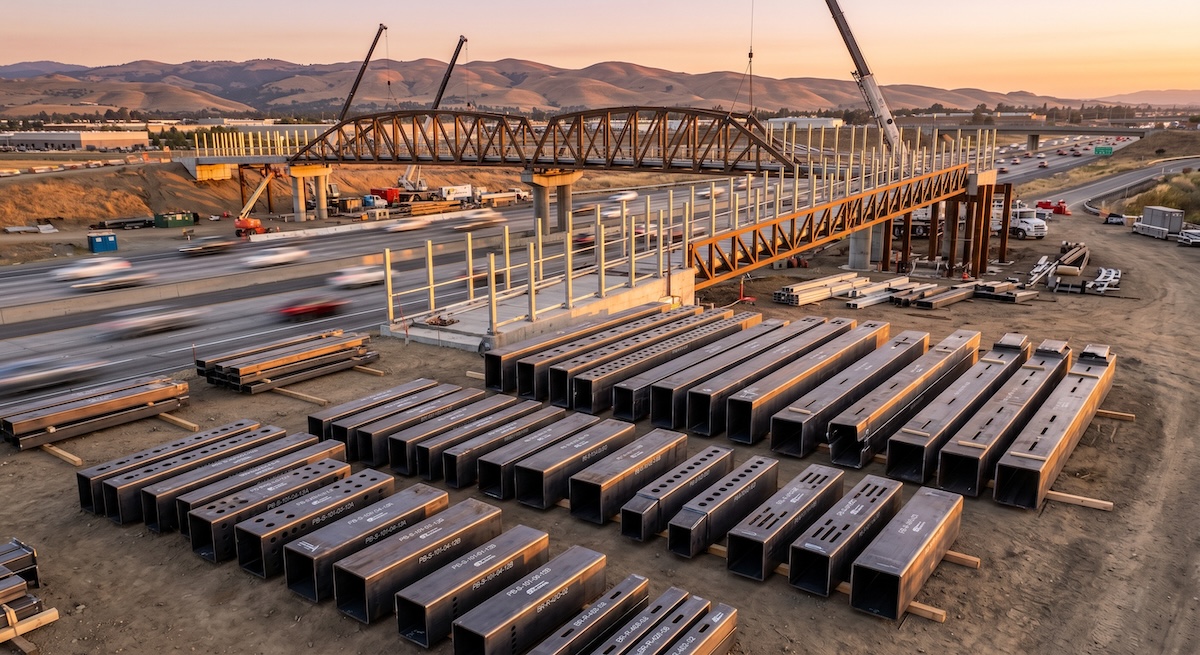
Data center supports are the steel frames, brackets and mounting structures that hold equipment, piping and cooling infrastructure in place. Blueline's data center service page lists structural supports and equipment mounting systems among its applications. A tube laser suits this work because one program cuts every feature, which keeps repeat parts consistent.
Support parts are usually built from square, rectangular or round tube. Blueline's site says it processes square, rectangular, round and oval tube, plus structural profiles such as angle, channel and C-channel.
On the equipment side, Blueline's LT7 tube lasers are 4kW machines that handle up to 6 inch square or round tube and run fully automatic. The shop also states it can process tube up to 13 inch diameter with 5-axis beveling capability.
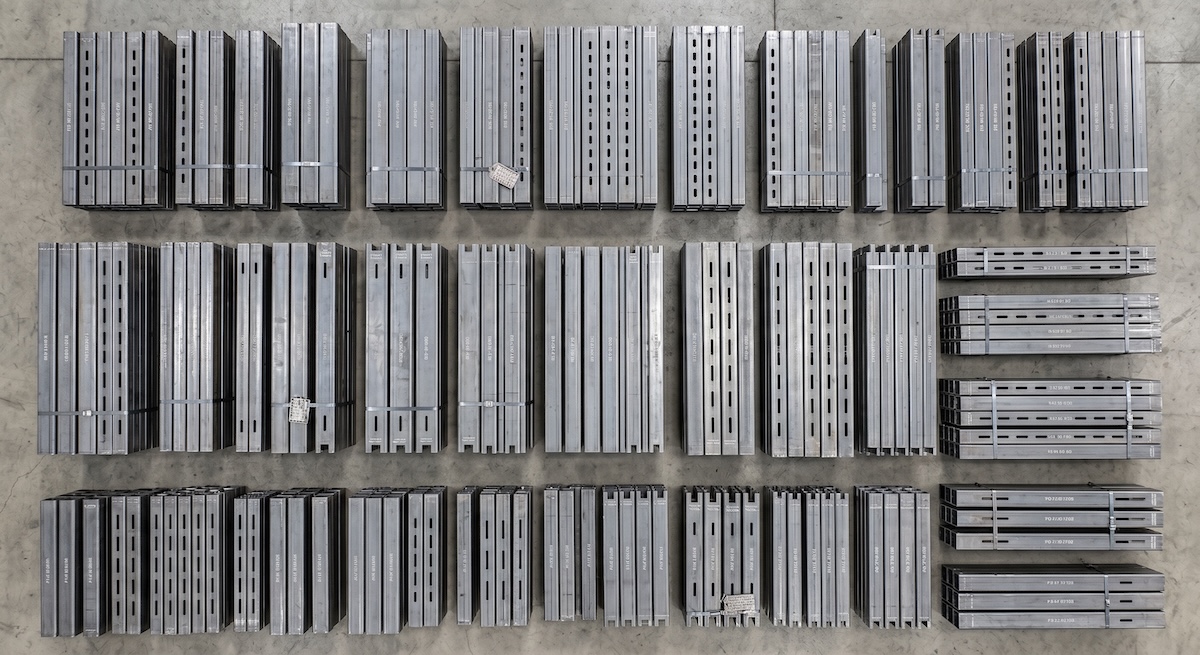
Repeatability matters more on supports than on most parts. A data center job can call for hundreds of near-identical brackets and frames. When each one comes off the same program, the field crew is not sorting out small differences on site.
How do tab and slot features cut down support assembly time?
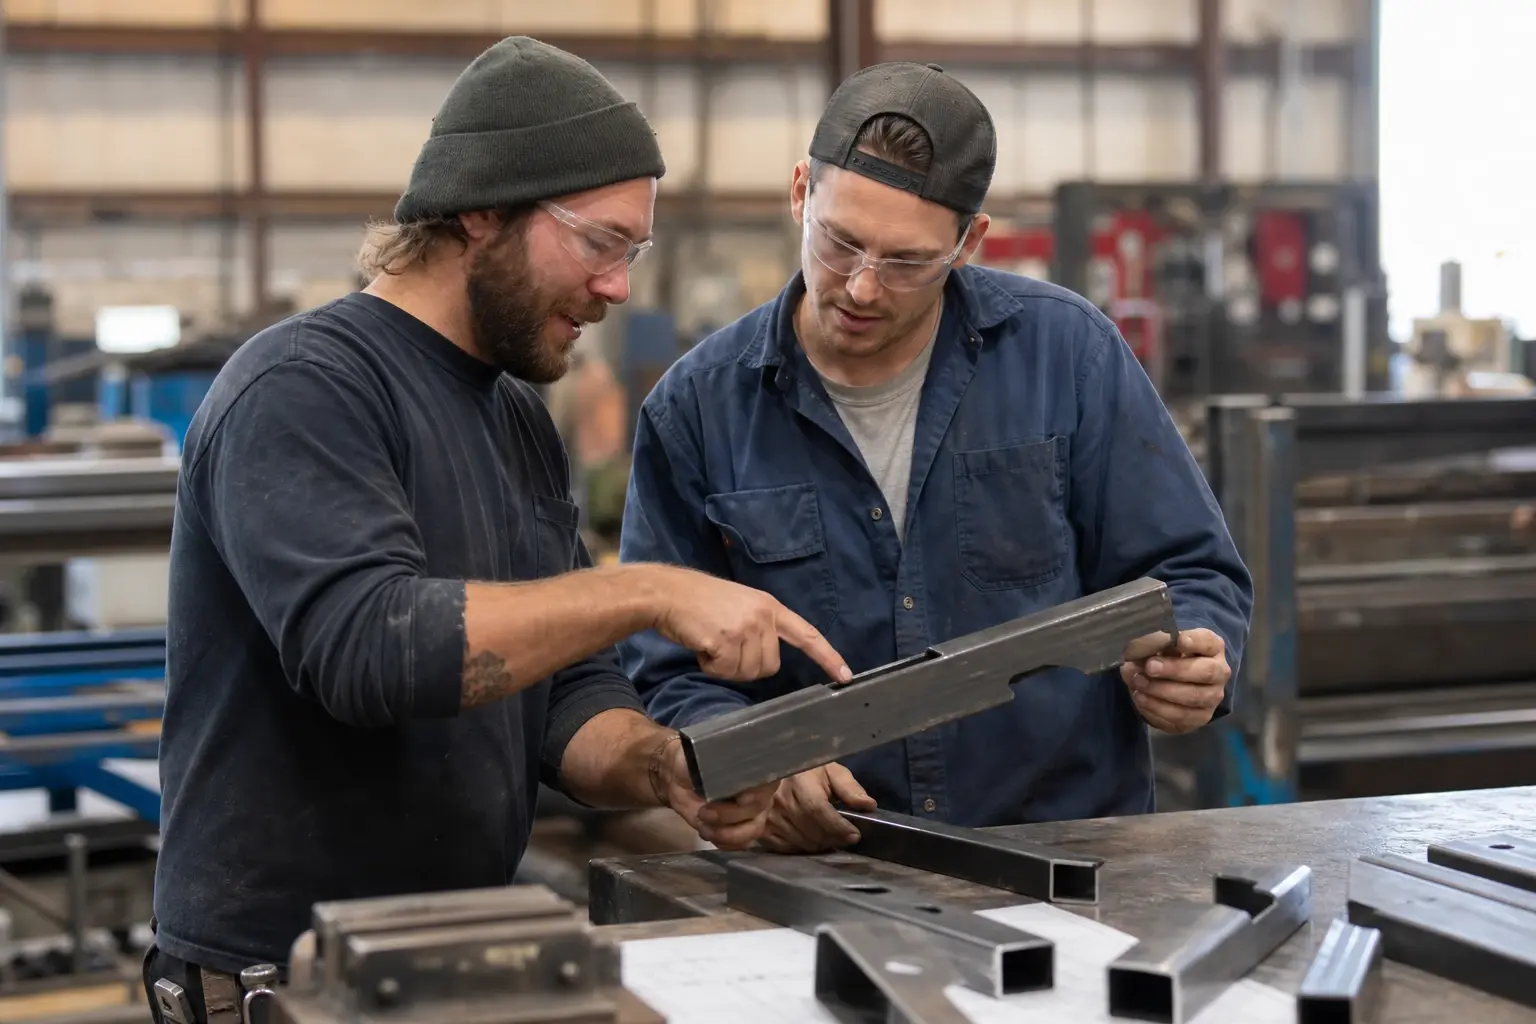
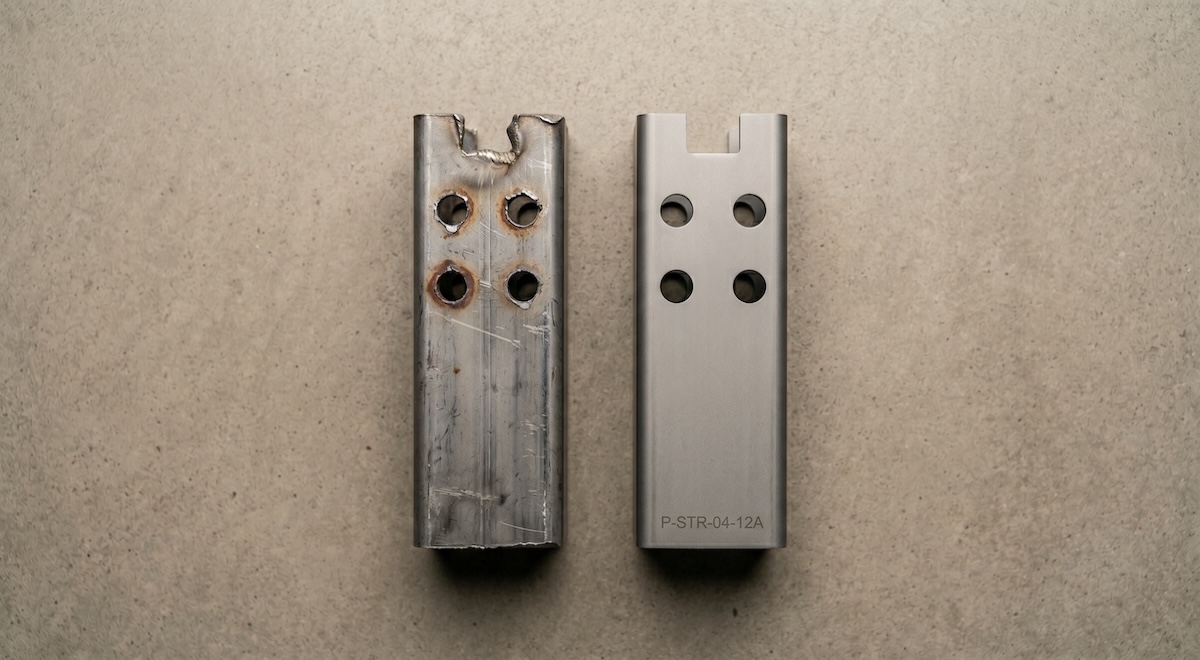
Tab and slot design puts a protruding tab on one part into a matching slot on the mating part, so the parts locate themselves during assembly. A tube laser cuts both features in the same program as the tube itself. The result is fewer jigs and less measuring before welding.
Micron's guide to self-fixturing welded assemblies describes the idea as "creating interlocking geometric features that position components automatically during assembly." That guide is written around sheet and plate work, but the same logic carries over to tube.
What tab and slot design asks of you
You need to plan the fit before the parts are cut. Leave enough clearance for the material and any coating. Tell the shop which joints are critical so the tab geometry matches the load path.
Welding usually still makes the joint structural. The tabs locate the parts. Confirm the weld plan with your fabricator before finalizing the drawing.
Why single-operation cutting helps
Every extra machine or setup adds a chance for error. Blueline states that single-operation processing reduces error rates by up to 70%. Cutting the length, slots and holes in one pass is the reason. Read that as Blueline's own claim, not an industry benchmark. See Blueline's precision slotting, notching and hole cutting service for the features it cuts.
What should a support drawing include before you ask for a quote?
Include a dimensioned drawing or 3D model, the tube size and wall thickness, the material grade, the quantity, and any finish or coating. Mark which features are critical to fit. Complete files let the shop quote without back and forth and reduce the odds of a wrong cut.
| Item to send | What to include | Why it matters |
|---|---|---|
| Geometry | Dimensioned drawing or 3D model with every slot, notch and hole | One program cuts all features, so missing details mean rework |
| Tube spec | Shape, outside dimensions, wall thickness | Sets machine fit and cutting parameters |
| Material | Carbon steel or stainless, and grade | Changes fit clearance, finish and handling |
| Quantity | Prototype count, first release, or repeat volume | Shapes the plan for programming and batching |
| Finish | Paint, coating or passivation needs | Coatings can affect tab and slot clearance |
| Critical fits | Which joints and holes control assembly | Tells the shop where accuracy matters most |
If a design is still moving, ask for a short run first. Blueline's custom tube prototyping and short-run fabrication service exists for that step.
Does stainless change how you design support parts?
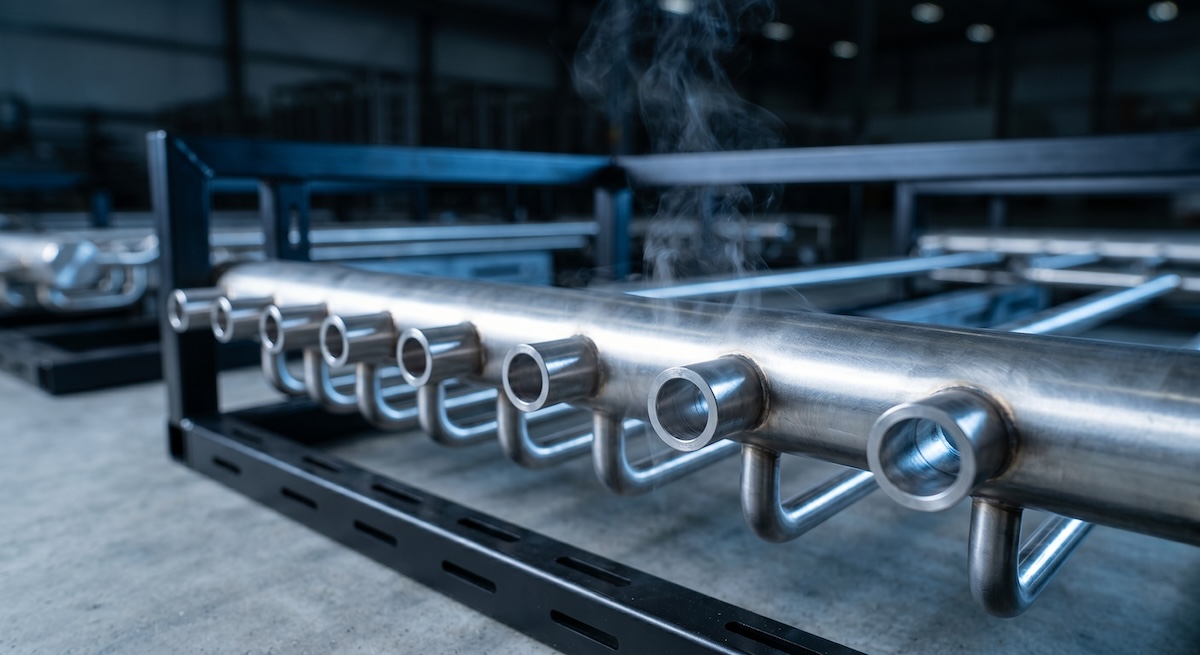
Yes, mainly in fit clearance and finish. Stainless is often chosen where corrosion resistance matters, such as cooling lines. Micron's guide notes that stainless assemblies need larger tab and slot clearances than steel to avoid galling. Confirm the clearance with your fabricator for the exact grade.
| Factor | Carbon steel supports | Stainless supports |
|---|---|---|
| Typical use | Structural frames, equipment mounts | Cooling infrastructure, corrosion-sensitive areas |
| Fit clearance | Standard tab and slot clearance | Often larger clearance to avoid galling |
| Finish | Usually painted or coated | Often left as-is or passivated, per spec |
| What to tell the shop | Coating type and thickness | Grade and finish requirement |
Blueline states that its programs, feed rates and material handling are already tuned for sustained stainless production. For a deeper look at stainless and schedule, read Blueline's post on stainless steel fabrication for data centers.
A verified example: 16 truckloads of stainless for a Sacramento cooling project
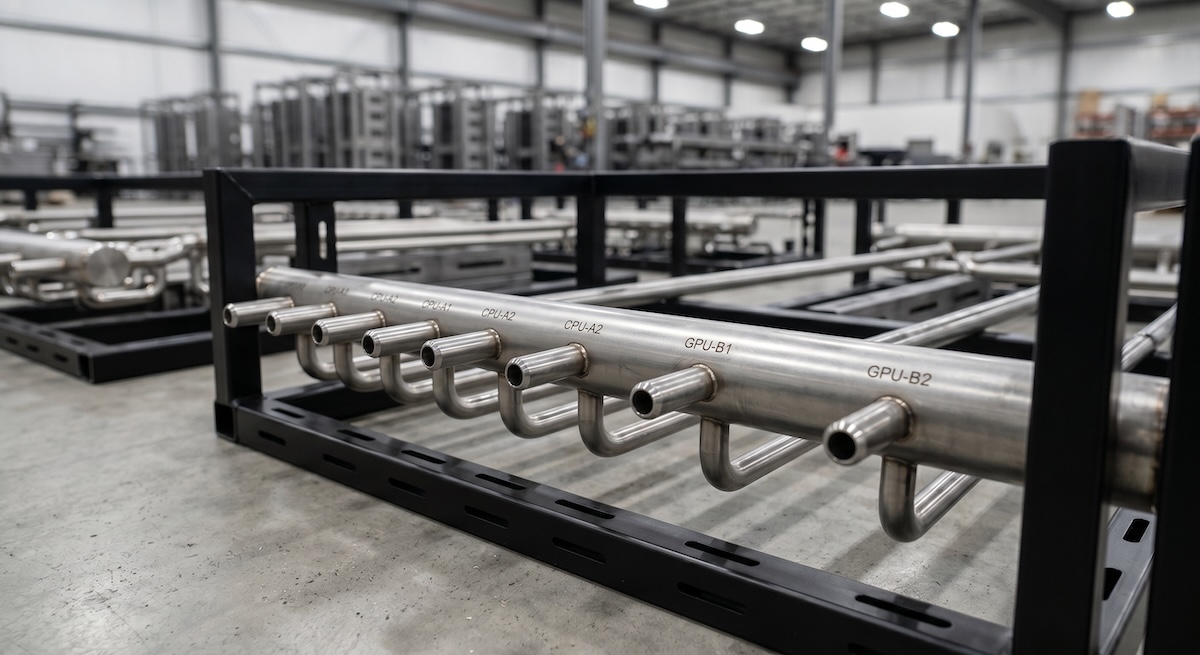
In 2025, Blueline processed 16 truckloads of stainless steel for an AI data center cooling project in Sacramento. Blueline's page lists this project alongside its data center work. The details below are general lessons, not extra project facts.
At that scale, repeatability is the whole game. Parts cut from one program match each other, which keeps assembly predictable. It also makes a complete drawing package worth the time up front.
Frequently asked questions
What tube sizes can Blueline cut for supports?
Blueline's LT7 tube lasers handle up to 6 inch square or round tube and run fully automatic. The site also states processing of tube up to 13 inch diameter with 5-axis beveling capability. Send your exact size and wall for confirmation.
Can tab and slot parts still be welded?
Yes. In most designs the tabs locate the parts and welding makes the joint structural. Confirm the weld plan and fit clearance with your fabricator before you release the drawing.
What files does Blueline need to quote support parts?
Send a dimensioned drawing or 3D model with tube size, wall thickness, material grade, quantity and finish. Ask the shop which file formats it prefers. Complete information reduces questions and rework.
Does Blueline ship to data center sites outside California?
Blueline has one facility, in Chino, CA. It ships to and serves Portland, Tucson, San Francisco, San Diego, Seattle, Salt Lake City, Las Vegas, San Jose and Los Angeles.
Can I order a prototype before a full release?
Yes. Blueline offers custom tube prototyping and short-run fabrication. A short run lets you check fit before committing to volume.
Get supports that fit the first time
Good support parts start with a complete drawing and a clear fit plan. Blueline's tube lasers do the rest from Chino, CA.
Get a Quote or call (951) 833-5597.