Quick Summary
- A tube laser adds heat to the cut edge. A waterjet is a cold process.
- Published comparisons say laser is typically faster on thinner metal, and waterjet handles much thicker stock and non-metals.
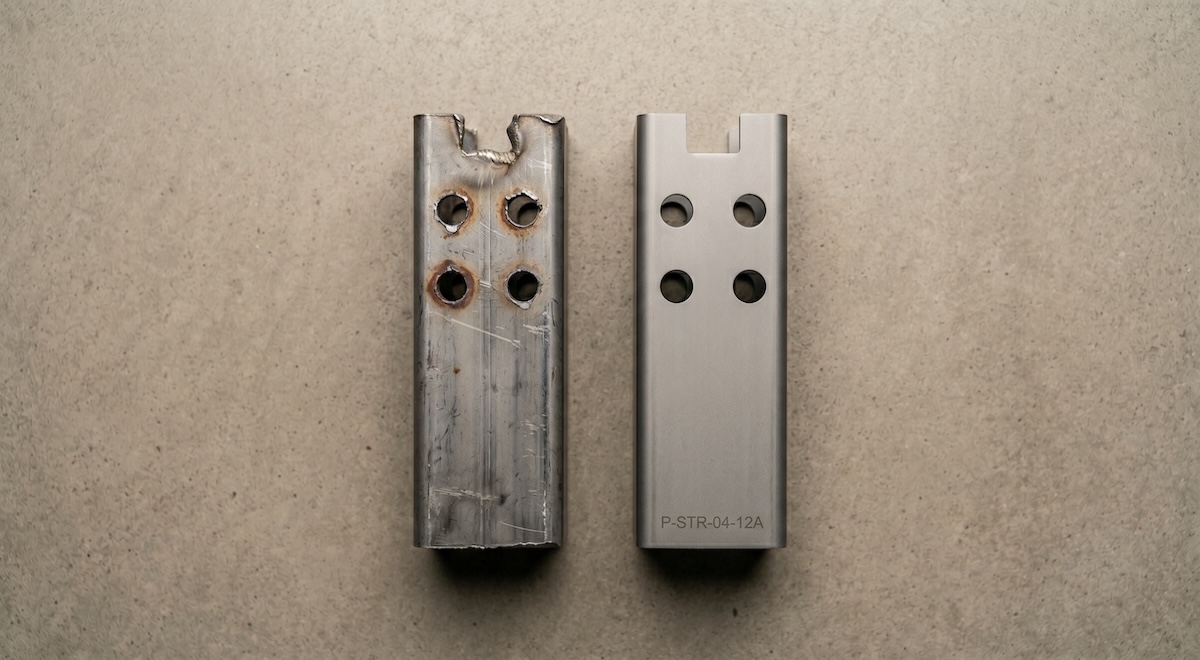
- Tube parts with many slots, notches and holes often suit a tube laser, because one operation can cut all of them.
- Choose by material, thickness, heat tolerance and feature count, not by habit.
A tube laser is often the better fit for steel tube parts that need slots, notches and holes. Waterjet fits very thick stock, non-metals and jobs that cannot accept any heat. Blueline Industries runs tube laser cutting from its shop in Chino, CA, so this guide is about fit, and it says plainly when waterjet is the right call.
The comparisons published online mostly cover flat material. Tube adds its own constraints, so treat the sourced points below as a starting frame and send your part for a real answer.

What is the difference between a tube laser and a waterjet?
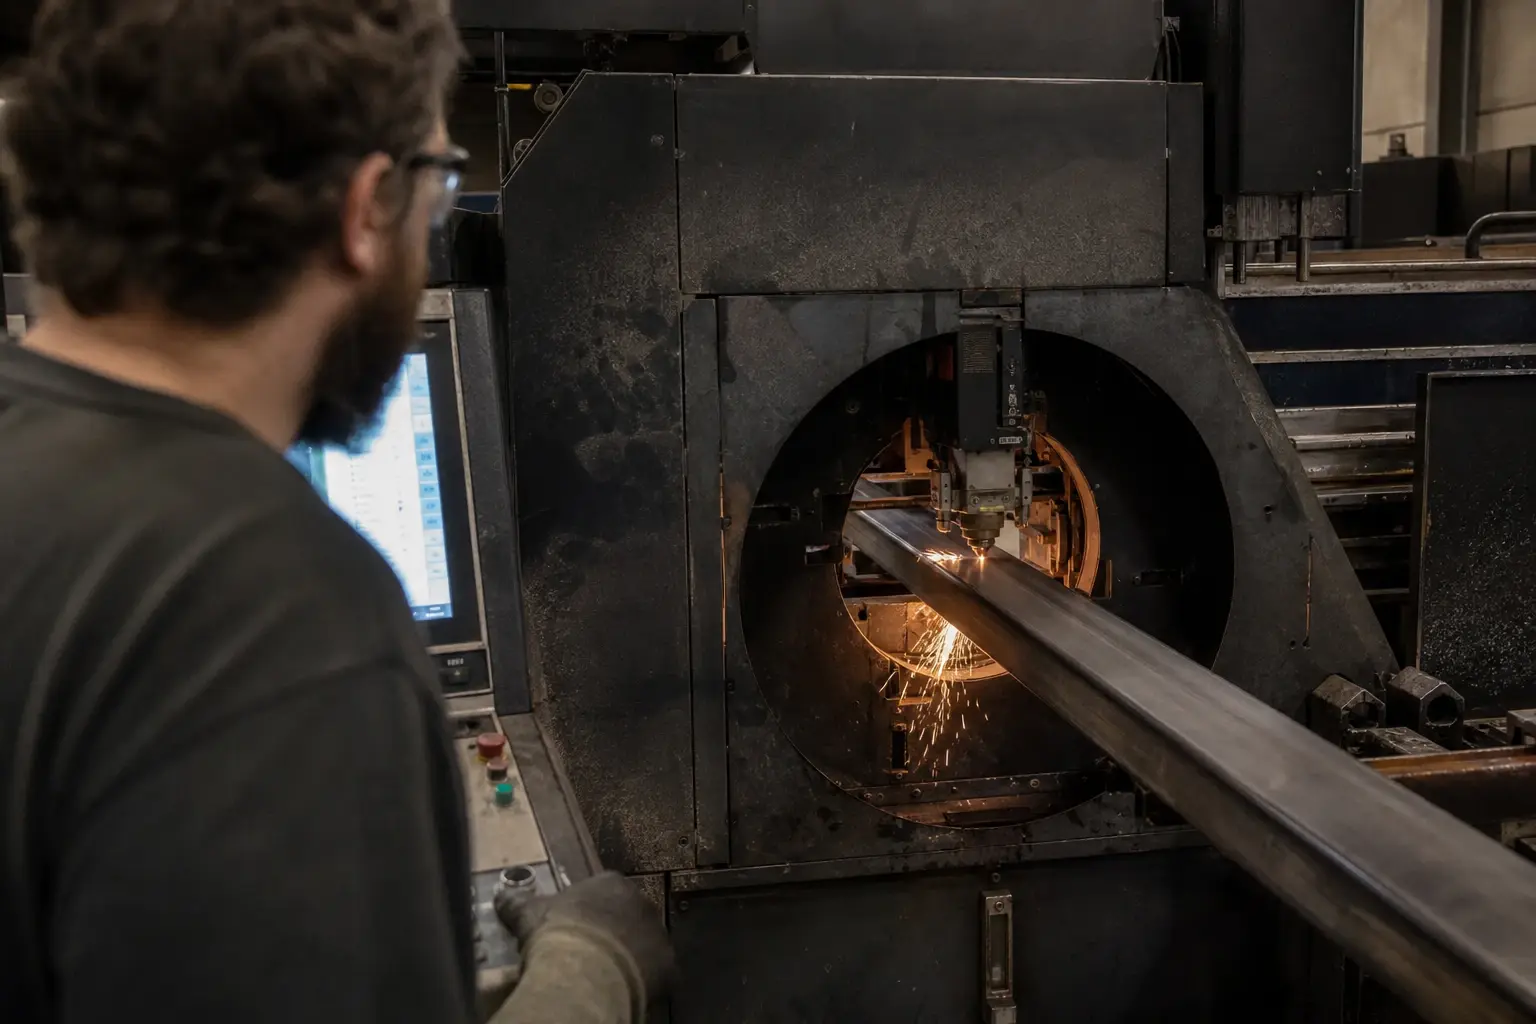
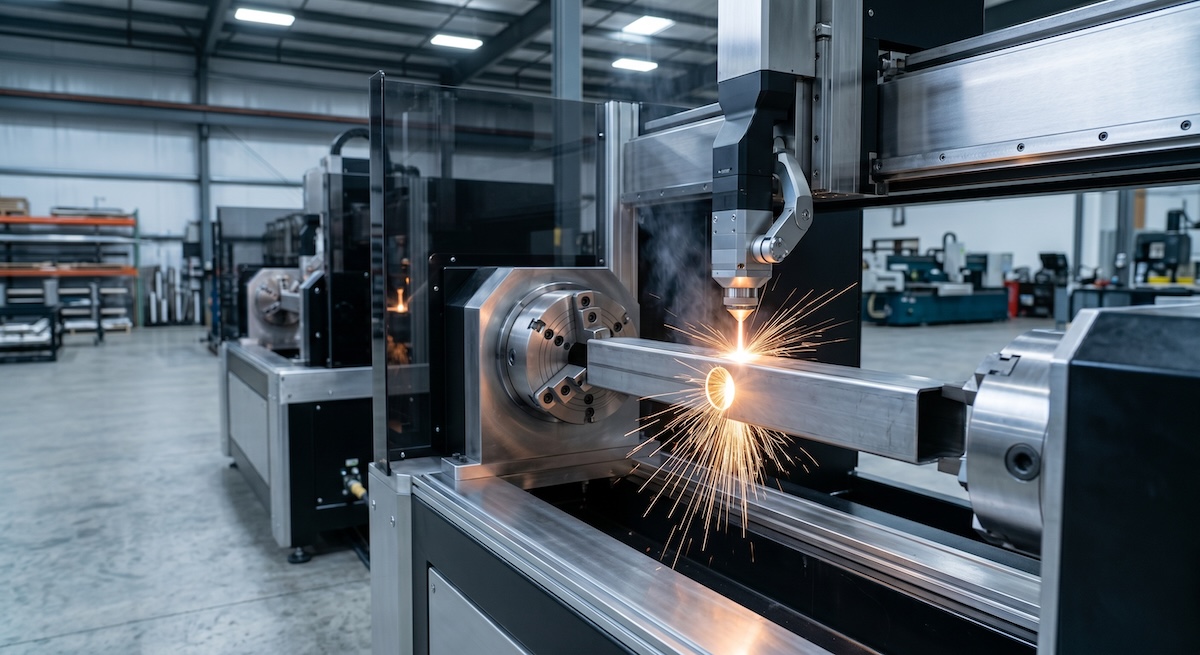
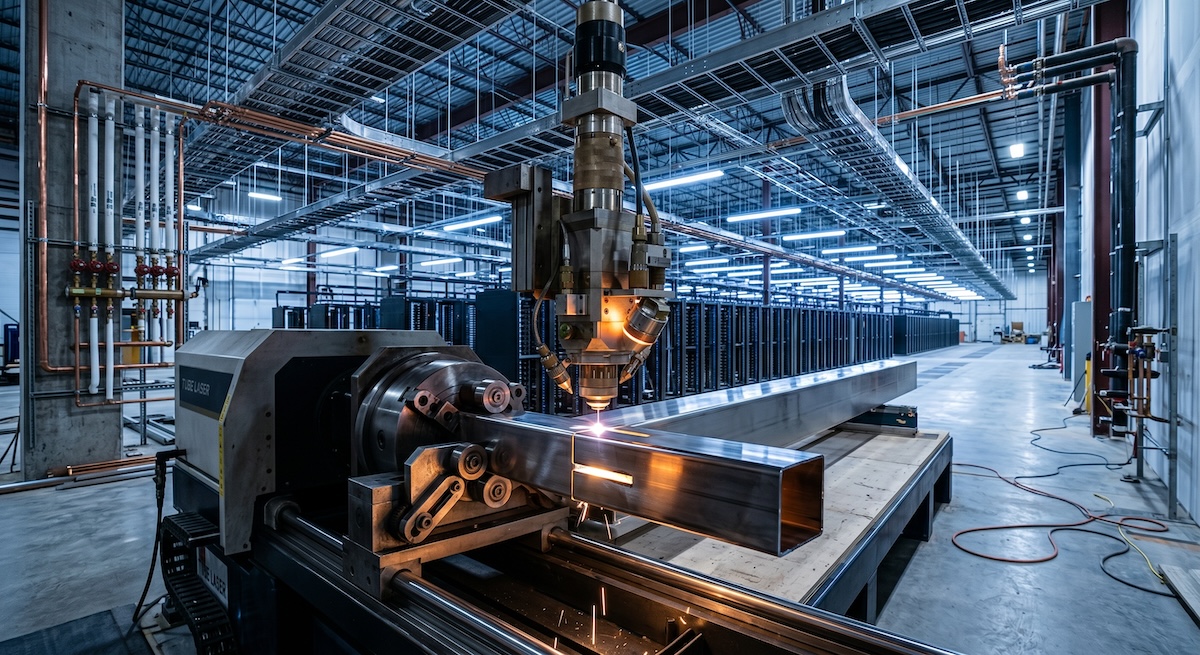
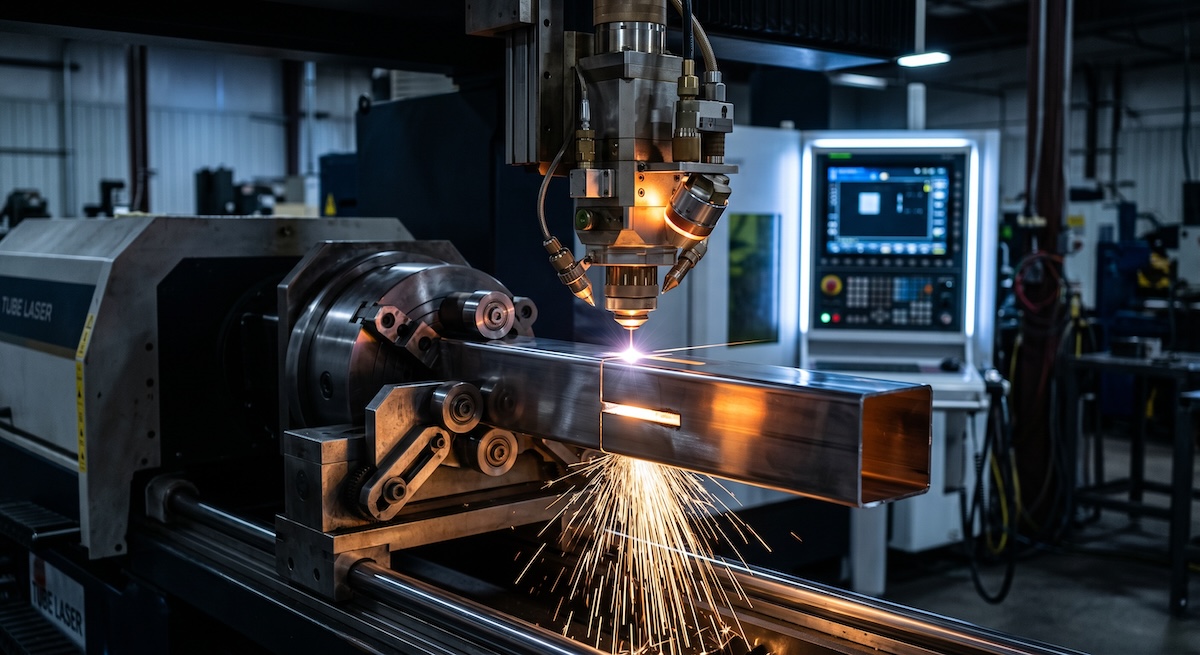
A tube laser melts and vaporizes steel with a focused beam, so it puts heat into the cut edge. A waterjet erodes material with high-pressure water and abrasive, so it is a cold process. That one difference drives speed, edge condition, material range and thickness limits.
Both are precise. Neither is better in every case. The right choice depends on what the part is made of and what it has to do.
How do speed and heat compare?
Published comparisons say laser cutting is typically faster than waterjet on thinner metal. They also say waterjet creates no heat-affected zone, while a laser can leave a narrow one along the edge. Blueline says its fiber laser produces a minimal heat-affected zone.
A heat-affected zone is the thin band of metal next to a cut whose properties the heat has changed. For many structural and fabrication jobs that band is not a concern. For a part with a strict no-heat requirement, it can be.
Check your drawing notes. If the spec does not mention heat effects, ask the designer whether it matters.
What can a waterjet do that a tube laser cannot?
Waterjet cuts nearly any material, including glass, stone and composites, and it handles much thicker stock. One published comparison says waterjet can cut material up to 6 inches thick. If your part is non-metal or very thick, waterjet is the better call.
The same comparison notes a limit: a waterjet cannot make sharp inside corners, because the corner radius is roughly the width of the jet. A laser beam is narrower, so it does not share that limit.
Blueline's focus is metal tube. We would rather tell you when a part belongs on another machine than quote it.
FactorTube laserWaterjetHeat at the cut edgeAdds heat, narrow heat-affected zoneNone, cold processSpeed on thinner metalTypically fasterSlowerMaterial rangeMetals, including steel and stainlessNearly any materialThick stockSpeed drops as thickness growsCuts up to 6 inches in one published comparisonInside cornersSharpRadius about the width of the jet
Where does a tube laser win on tube parts?
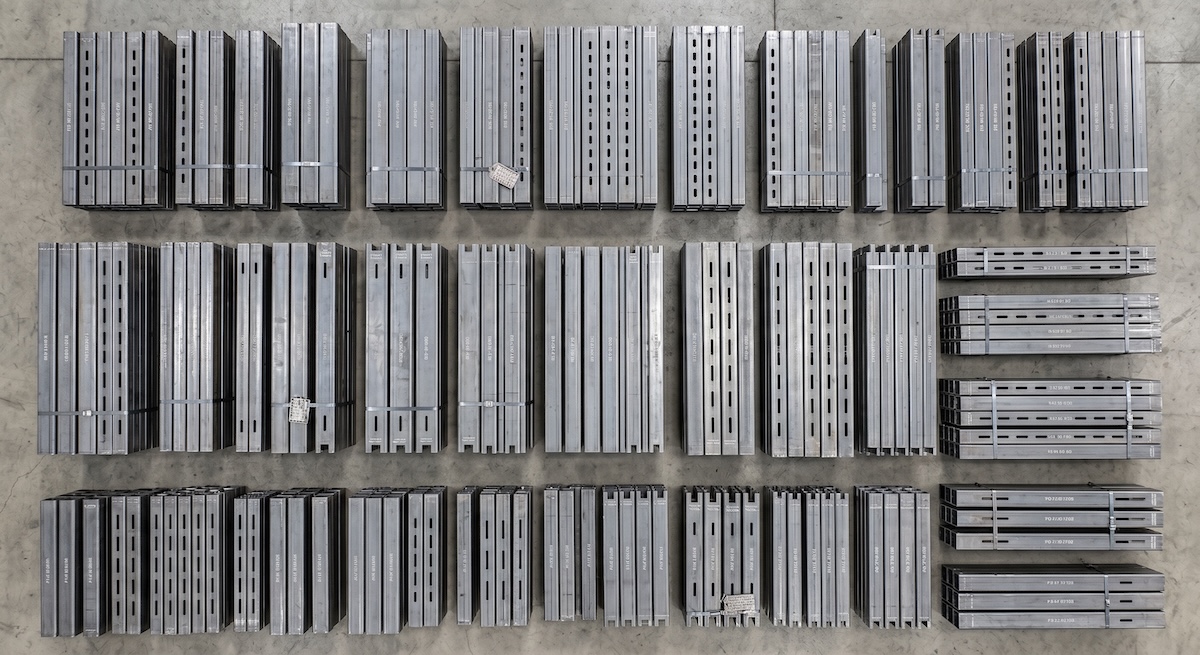
A tube laser wins when a tube part carries many features and the volume is real. Blueline cuts, slots, notches and drills tube in one operation, so the part does not move between machines. Fewer moves mean fewer chances for stacked tolerance error.
According to Blueline, tolerances are plus or minus 0.003 inch. Blueline states that single-operation processing reduces error rates by up to 70%. Both are Blueline's own claims, so confirm them against your drawing.
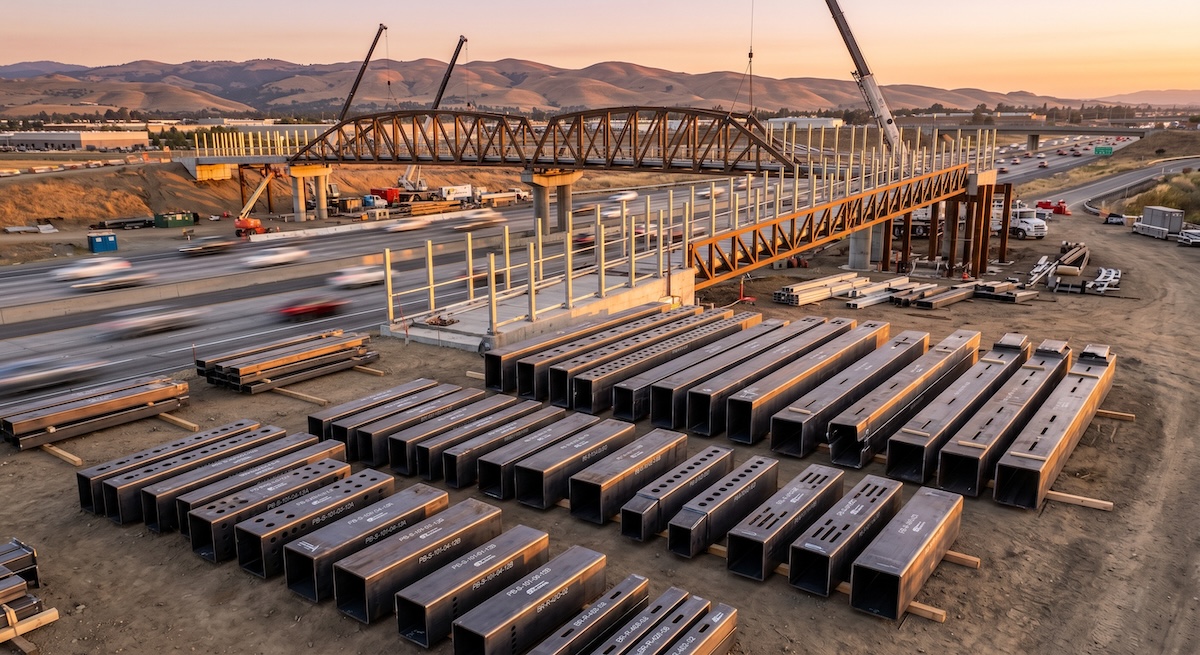
Scale matters too. In 2025, Blueline processed more than one million pounds of steel for the Coachella Sahara Stage. At that size, process time per part adds up quickly. See the steel tube laser cutting and slotting, notching and hole cutting pages for what Blueline cuts.
If you are also weighing plasma, read Tube Laser vs Plasma Cutting: Which Fits Your Tube Job?
One caution on the published numbers. The sources compare the processes on flat material, and vendors write some of them. Use them to frame the question, then check the answer against your own drawing.
How should you choose between them?
Work through five questions in order. If the first one rules out the laser, stop there. If it does not, the later questions tell you how well the part suits one.
- Material. Is it steel, stainless or another metal? Non-metals point to waterjet.
- Thickness. Is the stock thin enough for a laser to run at speed? Very thick stock points to waterjet.
- Heat tolerance. Does the spec forbid any heat-affected zone? If so, ask the designer to confirm.
- Feature count. Does the part carry many slots, notches or holes? That favors a tube laser.
- Volume. Will you order the part repeatedly? Faster cutting on thinner metal helps most at volume.
A worked example, not a customer job
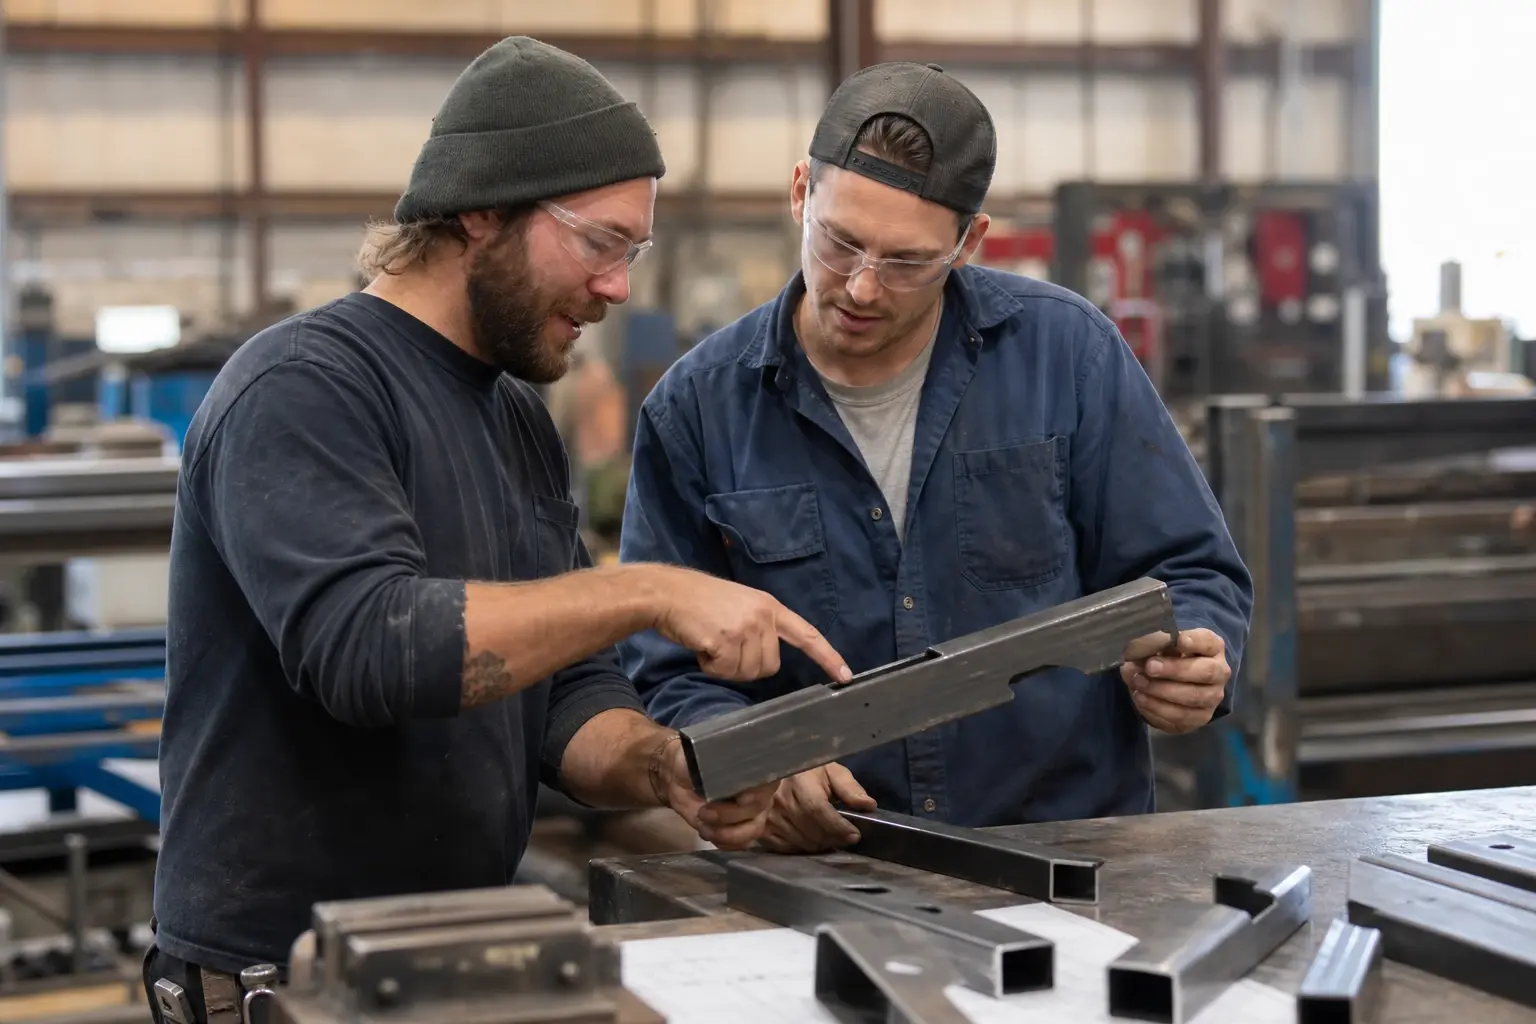
Picture a square steel tube with a dozen holes, several slots and a notched end. On a process that cuts one feature at a time, the part may visit a saw, a drill and a notcher. On a tube laser, one operation can cut every feature while the part stays clamped.
Now picture a thick plate with a complex outline and a no-heat note. That part belongs on a waterjet. The process follows the part, and the part does not follow the shop's favorite machine.
The question to ask any shop is simple: which of my parts do you cut best, and which should go elsewhere? A shop that answers honestly will save you a reorder.
Send the part, the material, the quantity and your heat requirement. Blueline will tell you whether it fits a tube laser. It will not stretch a quote to cover a part that belongs elsewhere.
Frequently Asked Questions
Is tube laser or waterjet more accurate?
Both are precise. One published comparison lists laser tolerances of 0.002 to 0.005 inch and standard waterjet tolerances of 0.005 to 0.015 inch, but that is for flat material and varies by setup. According to Blueline, its tube tolerances are plus or minus 0.003 inch. Confirm the figure for your part on the drawing.
Does a tube laser damage the metal?
A laser can leave a narrow heat-affected zone along the cut edge. Blueline says its fiber laser keeps that zone minimal. If your spec forbids any heat effect, say so when you quote.
Can a tube laser cut non-metals?
Blueline's work is on metal tube. Waterjet is the usual choice for glass, stone and composites.
What does Blueline need to quote a part?
Send the drawing or CAD file, material and grade, quantity and any heat or finish requirement. Blueline will confirm whether the part fits a tube laser.
Where is Blueline located?
Blueline operates from a single facility in Chino, CA. See the service area page for the cities it serves.
Pick the process the part needs
The right cut is the one that suits the material, the thickness and the spec. If your part is steel or stainless tube with real feature counts, send it to a shop that cuts it in one pass. Get a Quote or call Blueline at (951) 833-5597.