Quick Summary
- Pick the stainless grade from the coolant and water chemistry, not from habit. Grade 316 resists chlorides better than 304.
- The drawing should name grade, tube size, wall, cut features, tolerances and edge or cleaning needs before anyone quotes.
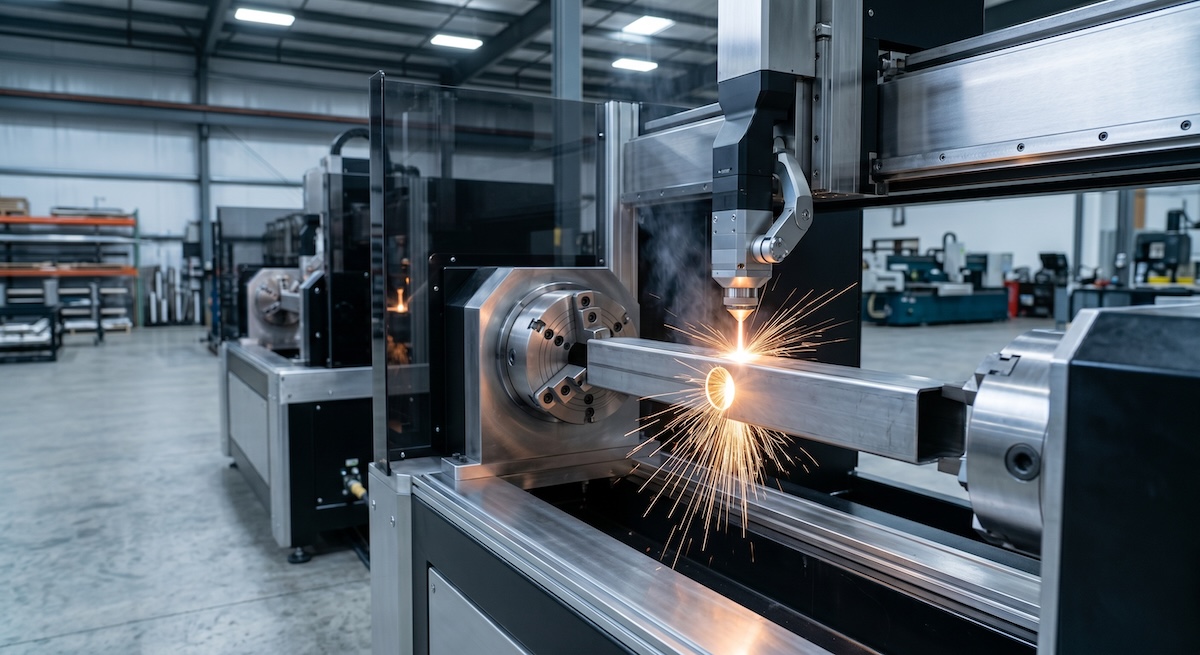
- One tube laser operation can cut slots, notches and holes in a single setup, which removes steps where errors creep in.
- Blueline Industries cuts stainless tube in Chino, CA and ships to buyers across the West.

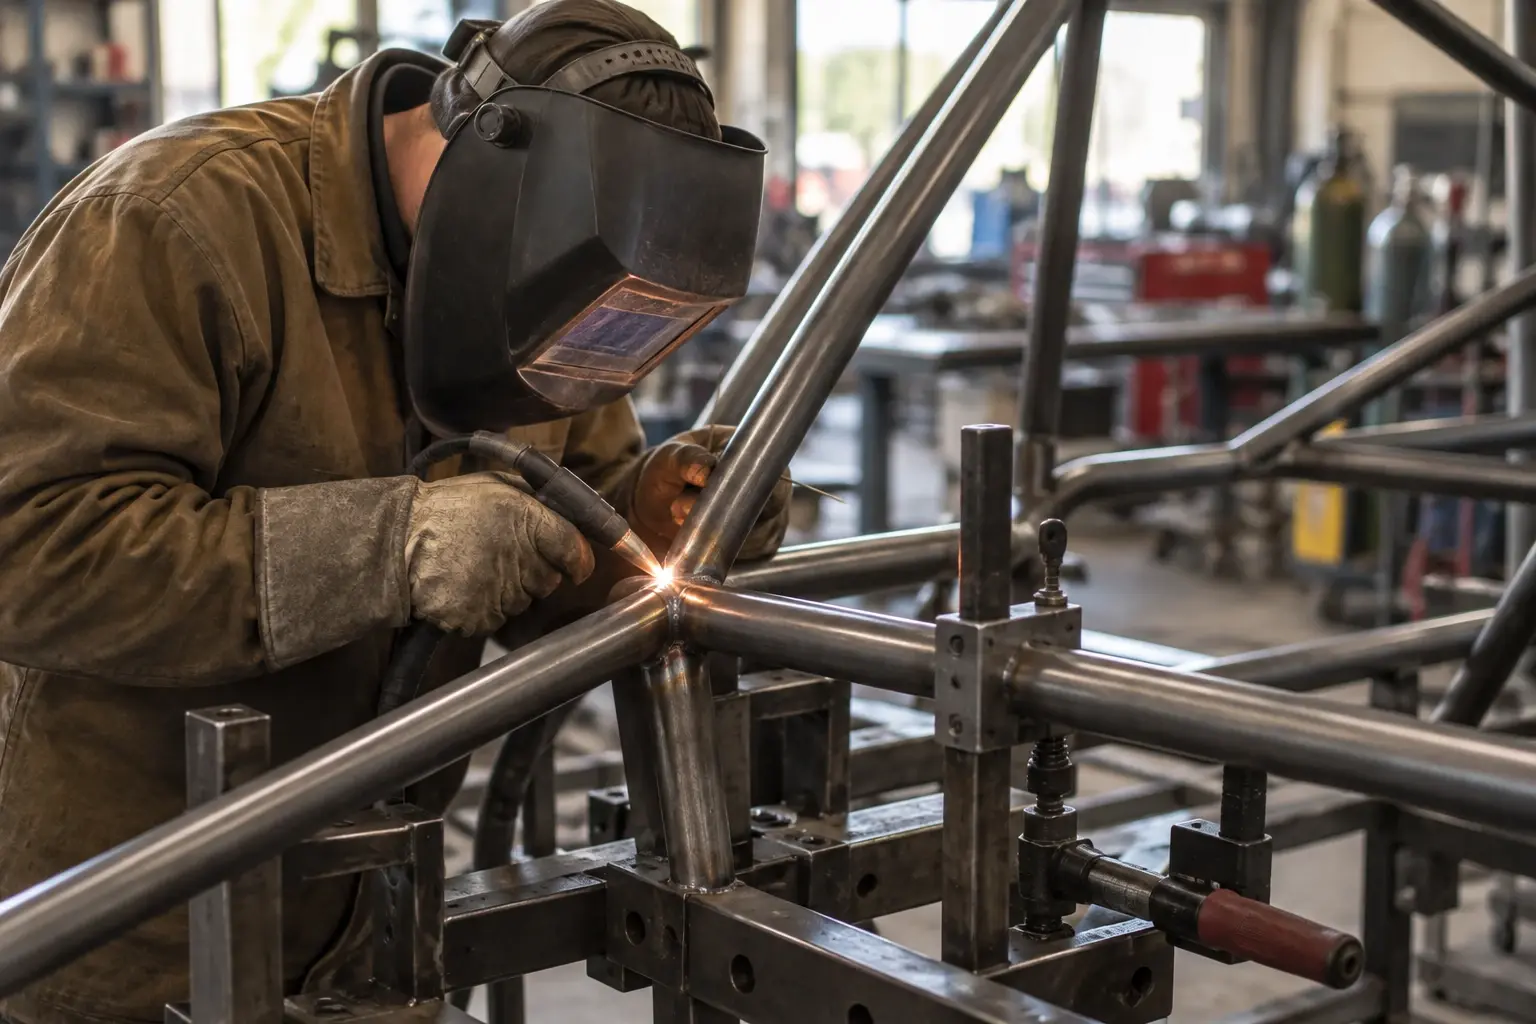
Stainless steel tube fabrication for cooling systems starts with one decision: which grade survives your water and coolant. At Blueline Industries, a tube laser cutting shop in Chino, CA, we cut what the drawing specifies, so the grade call belongs on the print before quoting begins.
This post covers how to choose between 304 and 316, what to put on a cooling tube drawing, and how single-operation tube laser cutting keeps fit-up tight. It is written for engineers and buyers who release stainless tube for data center cooling loops, skids and supports.
What stainless grade should a cooling system tube use?
Use 304 for clean, low-chloride freshwater service. Use 316 when the water or coolant carries chlorides or the loop runs warm. Type 316 contains 2 to 3% molybdenum, which improves resistance to pitting and crevice corrosion, according to Project Materials. Your engineer of record sets the grade.
Project Materials also reports that in chloride environments above 50 to 60 degrees C, type 304 is vulnerable to pitting and crevice attack, while type 316 gives more reliable service. Cooling loops rarely stay at one temperature, so a grade that is fine at the pump may not be fine at the hottest bend.
QuestionType 304Type 316Molybdenum contentLower than 3162 to 3%, per Project MaterialsChloride pitting and crevice resistanceLowerHigherTypical fitFreshwater systems and steam servicesBrackish water, chloride-bearing mediaStress corrosion cracking in chloridesSimilar to 316Similar to 304
That last row matters. Digital Refining notes there is no real difference between 304 and 316 in resistance to stress corrosion cracking. Moving to 316 does not fix every chloride risk, so the water chemistry and operating temperature still need an engineer's review.
Why does the cut edge matter on a coolant loop?
The cut edge is where stainless is most exposed to heat. Laser cutters use an assist gas to clear molten metal. Nitrogen is inert and prevents oxidation by displacing oxygen at the cut, according to Boss Laser. If your spec cares about edge condition, say so on the drawing.
Ask any shop which assist gas it uses for stainless and what edge finish to expect. Then ask what happens after cutting. If the print calls for cleaning, passivation or weld prep, list it as a separate line so it is quoted and scheduled, not assumed.
Keep the cut and the finish on separate lines
A cut part can still need cleaning, bending or welding before it goes into a loop. Writing each step as its own note keeps the quote honest and keeps the schedule clear.
What should a cooling tube drawing call out before you ask for a quote?
List grade, tube form, outside dimensions, wall thickness, length, every cut feature, tolerances, quantity and any finish or cleaning requirement. A drawing that names these items lets a shop quote once instead of asking five follow-up questions. Missing details are the usual cause of slow quotes.
- Grade and form: state 304 or 316 and whether you need round, square or rectangular tube.
- Size: outside dimensions and wall thickness, plus cut length.
- Cut features: slots, notches, holes and miters, with a clear datum for each.
- Tolerance: call out only the features that need it. Blueline states tolerances of plus or minus 0.003 inch, so ask which features that applies to.
- Edge and cleaning needs: any requirement beyond a standard cut.
- Documents: if you need material test reports, say so at quote time.
Send a 3D model or flat pattern with the PDF print when you have both. For a deeper checklist, see our guide on how to prepare CAD files for tube laser cutting.
Common drawing mistakes on cooling tube releases
Three mistakes show up again and again on stainless tube releases. Each one is easy to avoid when you catch it before quoting.
- Grade left open. A print that says "stainless" forces a shop to guess or stop and ask. Name the grade.
- Tolerances on every feature. Tight limits everywhere add inspection work. Mark the features that truly mate with other parts.
- Revisions mixed together. Send one current revision with a clear revision letter, so the cut file matches the print.
Fixing these on paper costs minutes. Fixing them after parts are cut costs material and schedule.
How does single-operation cutting help cooling tube assemblies?
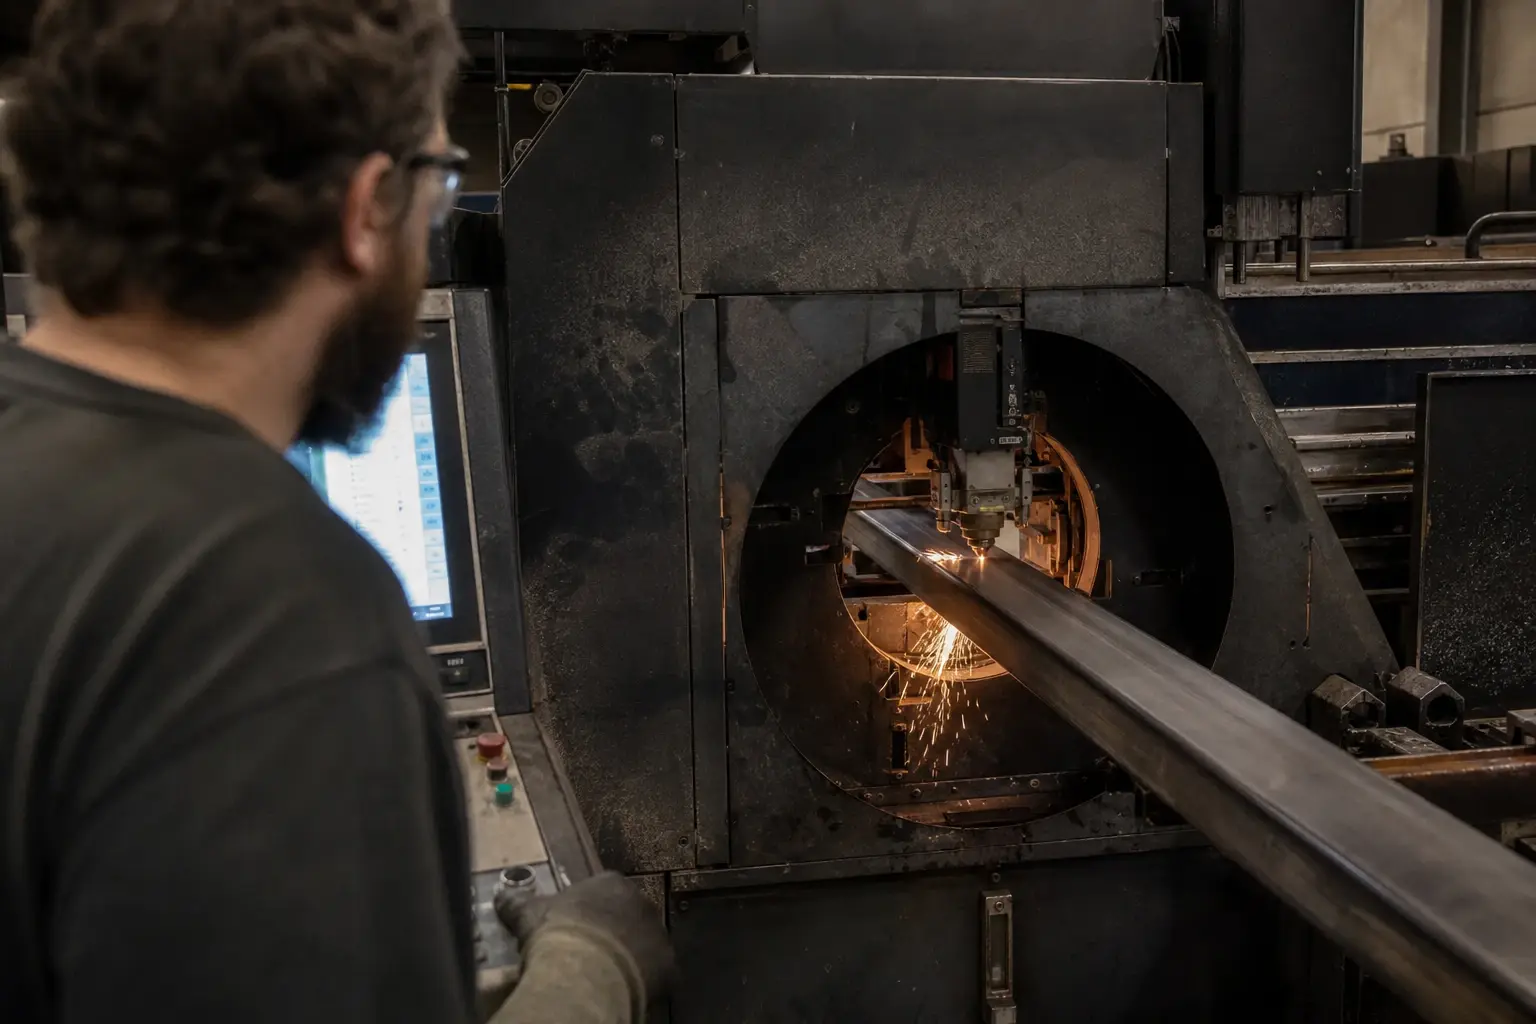
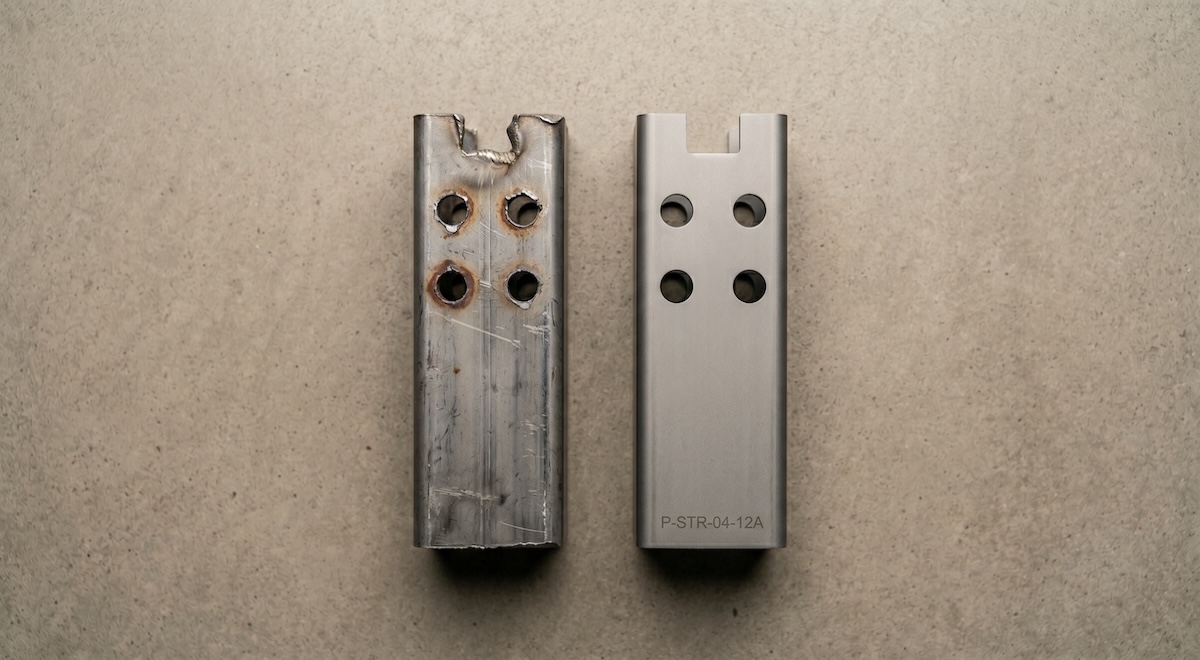
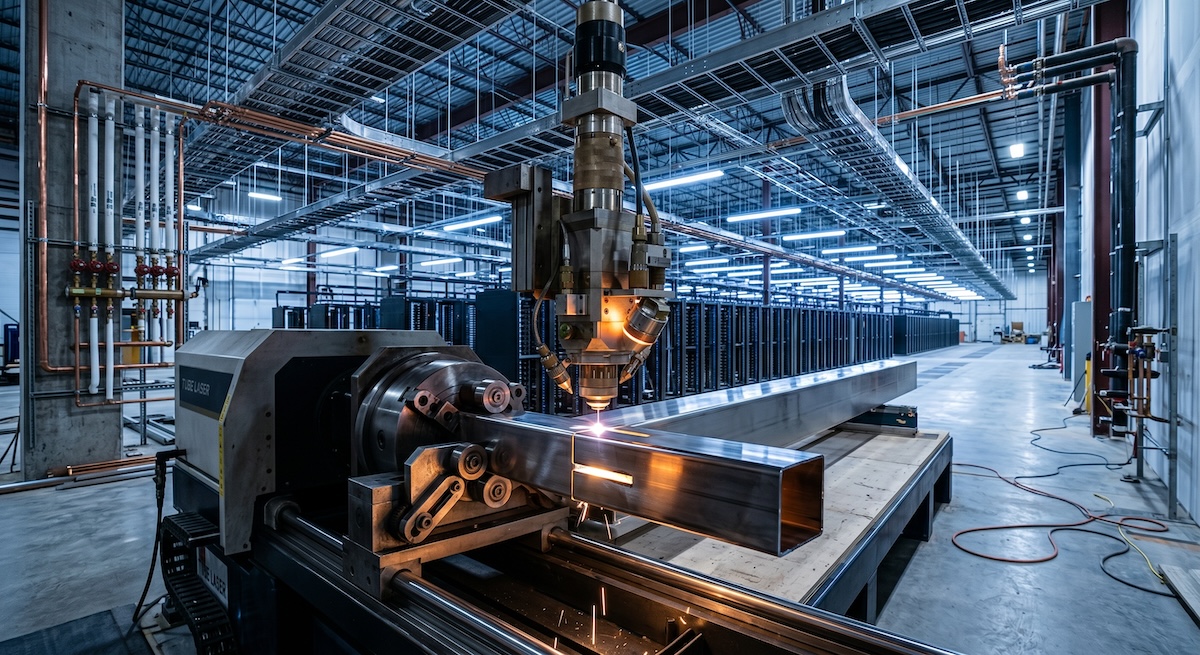
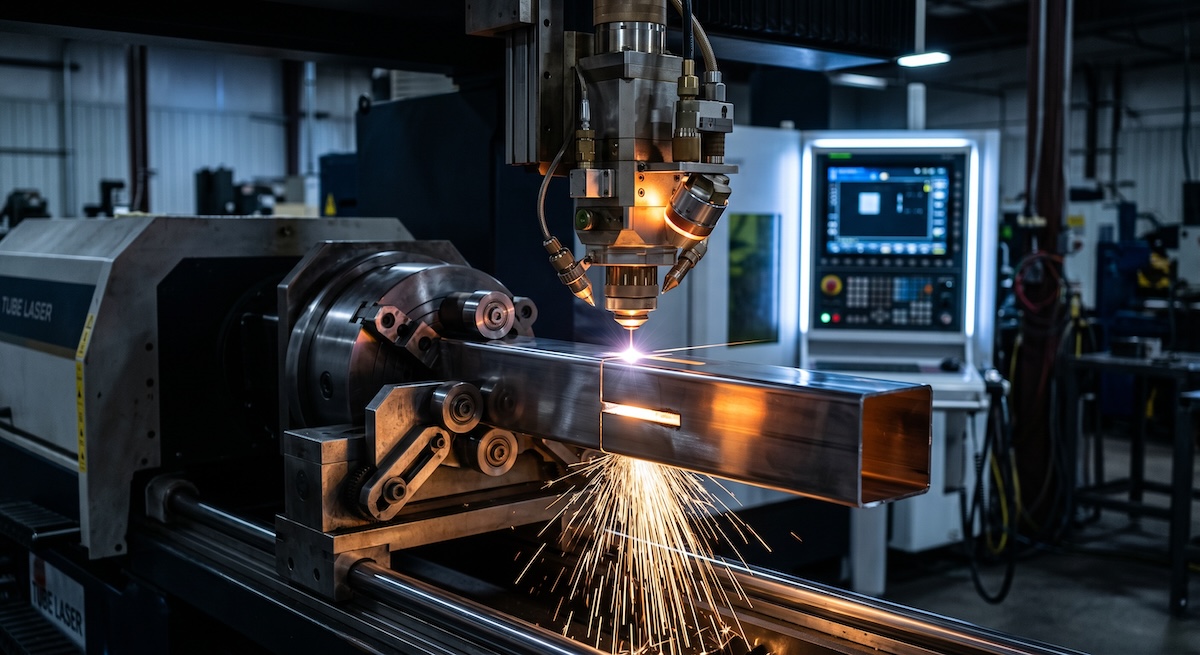
A tube laser can cut slots, notches and holes in one setup. Fewer setups mean fewer places for a part to drift out of position. Blueline states that single-operation processing reduces error rates by up to 70%. Parts arrive closer to ready for fit-up.
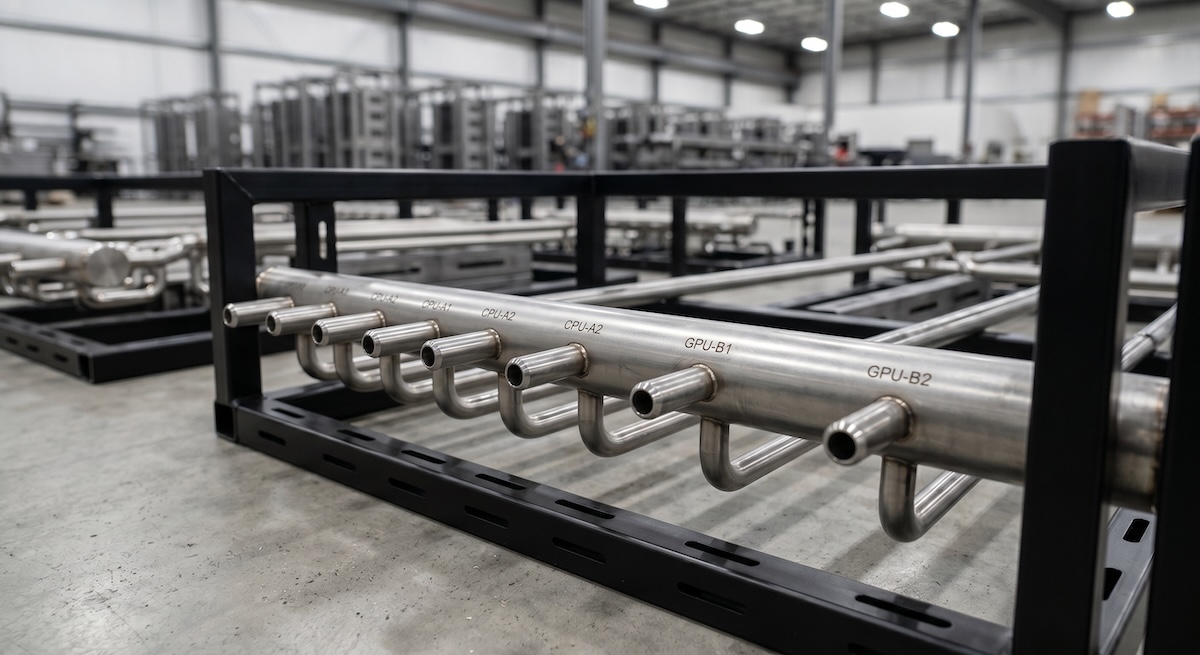
Blueline Industries runs LT7 tube lasers that handle up to 6 inch square and round tube, fully automatic, and processes tube up to 13 inch diameter. Cooling supports, manifold frames and skid members often combine many cut features on one length of tube, which is where one setup pays off.
Read more about our stainless steel tube processing and precision slotting, notching and hole cutting.
What does a real cooling project look like?
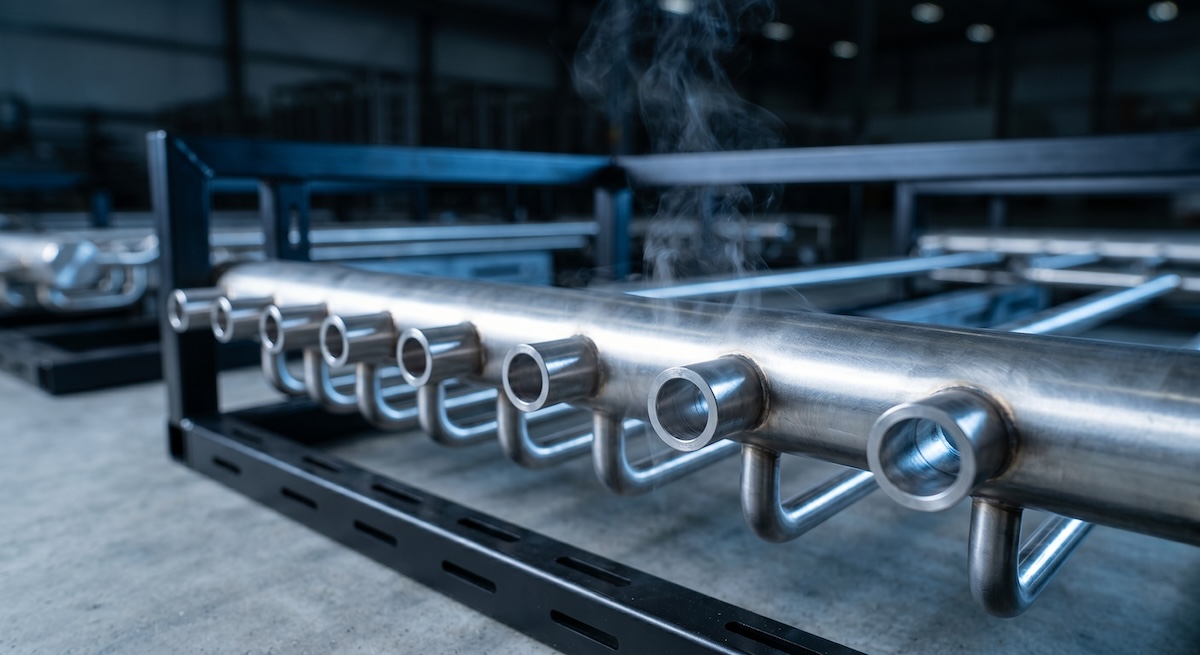
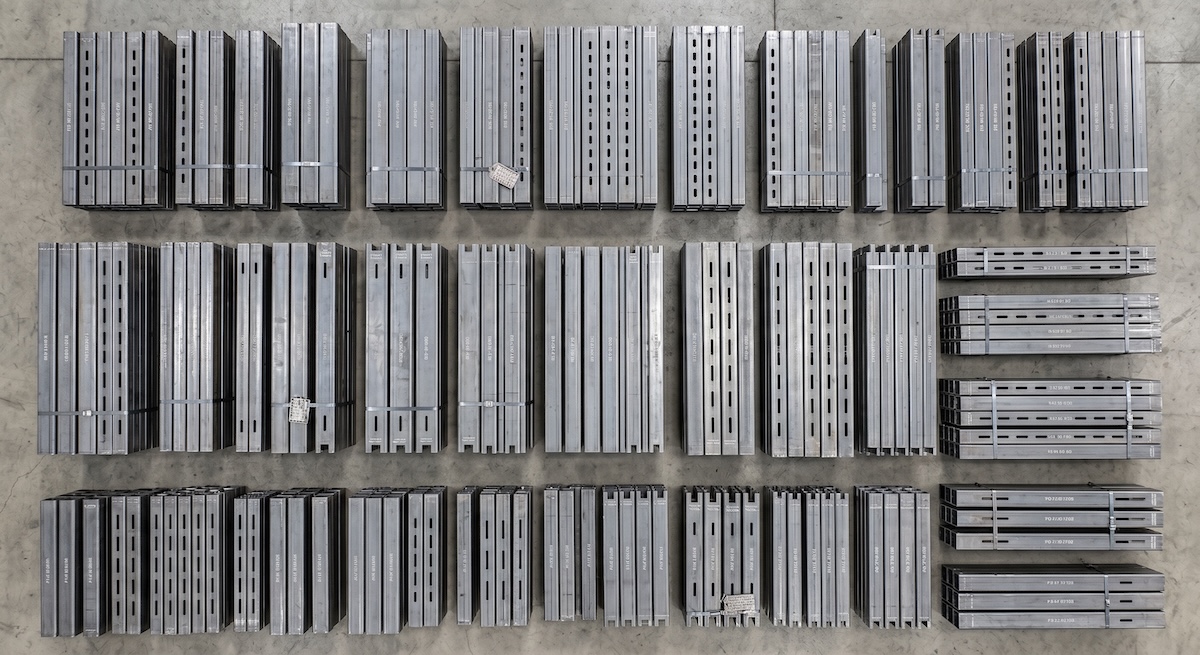
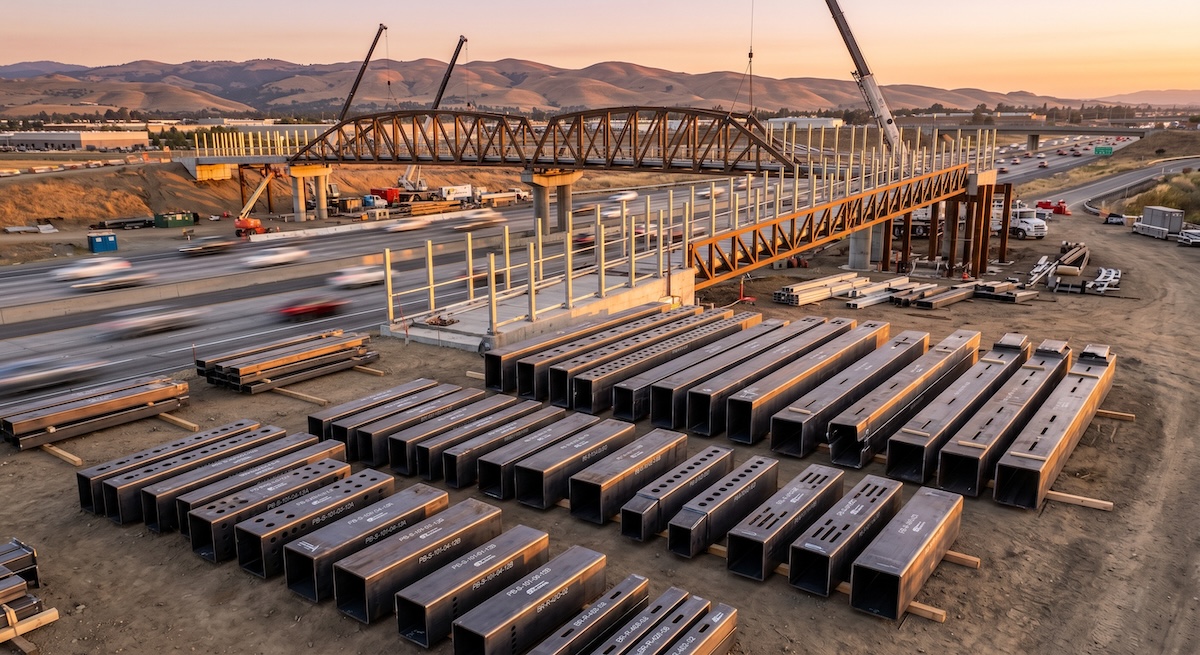
In 2025, Blueline Industries supplied stainless steel for an AI data center cooling project in Sacramento. The job moved 16 truckloads of stainless steel. The size of that order shows why drawing clarity matters: one unclear note repeated across a large release becomes a large problem.
For schedule-focused reading, see stainless steel fabrication for data centers. For the broader service picture, visit our data center and AI infrastructure services page.
Frequently Asked Questions
Is 316 always better than 304 for cooling systems?
No. Grade 316 resists chloride pitting and crevice attack better, but 304 can be the right call for clean freshwater service. Both behave similarly for stress corrosion cracking in chlorides. Your engineer should choose the grade from the actual fluid and temperature.
Can a tube laser cut stainless steel tube?
Yes. Blueline Industries processes stainless steel tube on its tube lasers at the Chino, CA facility. Share the grade, size and wall thickness with your quote request so the team can confirm the job fits the equipment.
How should I describe cleaning or passivation on the print?
List it as its own note, separate from the cut. Then ask Blueline during quoting which finishing steps it handles and which you arrange yourself, so the schedule reflects the real path of the parts.
What should I send with a stainless tube quote request?
Send the print or model, grade, tube size and wall, cut length, quantity, tolerances and any edge or cleaning needs. The more complete the package, the faster a quote can move.
Can Blueline run a short prototype before a large release?
Yes. Blueline offers custom tube prototyping and short-run fabrication. A small first run lets you check fit-up before you commit to a full release.
Send Your Cooling Tube Drawings to Blueline
Made in America, built on integrity. If your cooling system needs stainless tube cut right the first time, send us the print and we will tell you what we need to quote it. Get a Quote or call (951) 833-5597.