Quick Summary
A tube laser replaces the separate saw, drill and notching steps with one machine and one setup. For a part with holes, slots and angled ends, that usually means fewer stations and fewer handoffs. A saw and drill line still makes sense for simple square cuts.
This guide comes from Blueline Industries, a tube laser cutting shop in Chino, CA. It gives manufacturing engineers a way to compare the two routes one part at a time, instead of arguing about machines in general.
The answer depends on what the drawing asks for. Count the operations on the print, and the right route usually shows itself.
What is the difference between a tube laser and a saw-and-drill line?
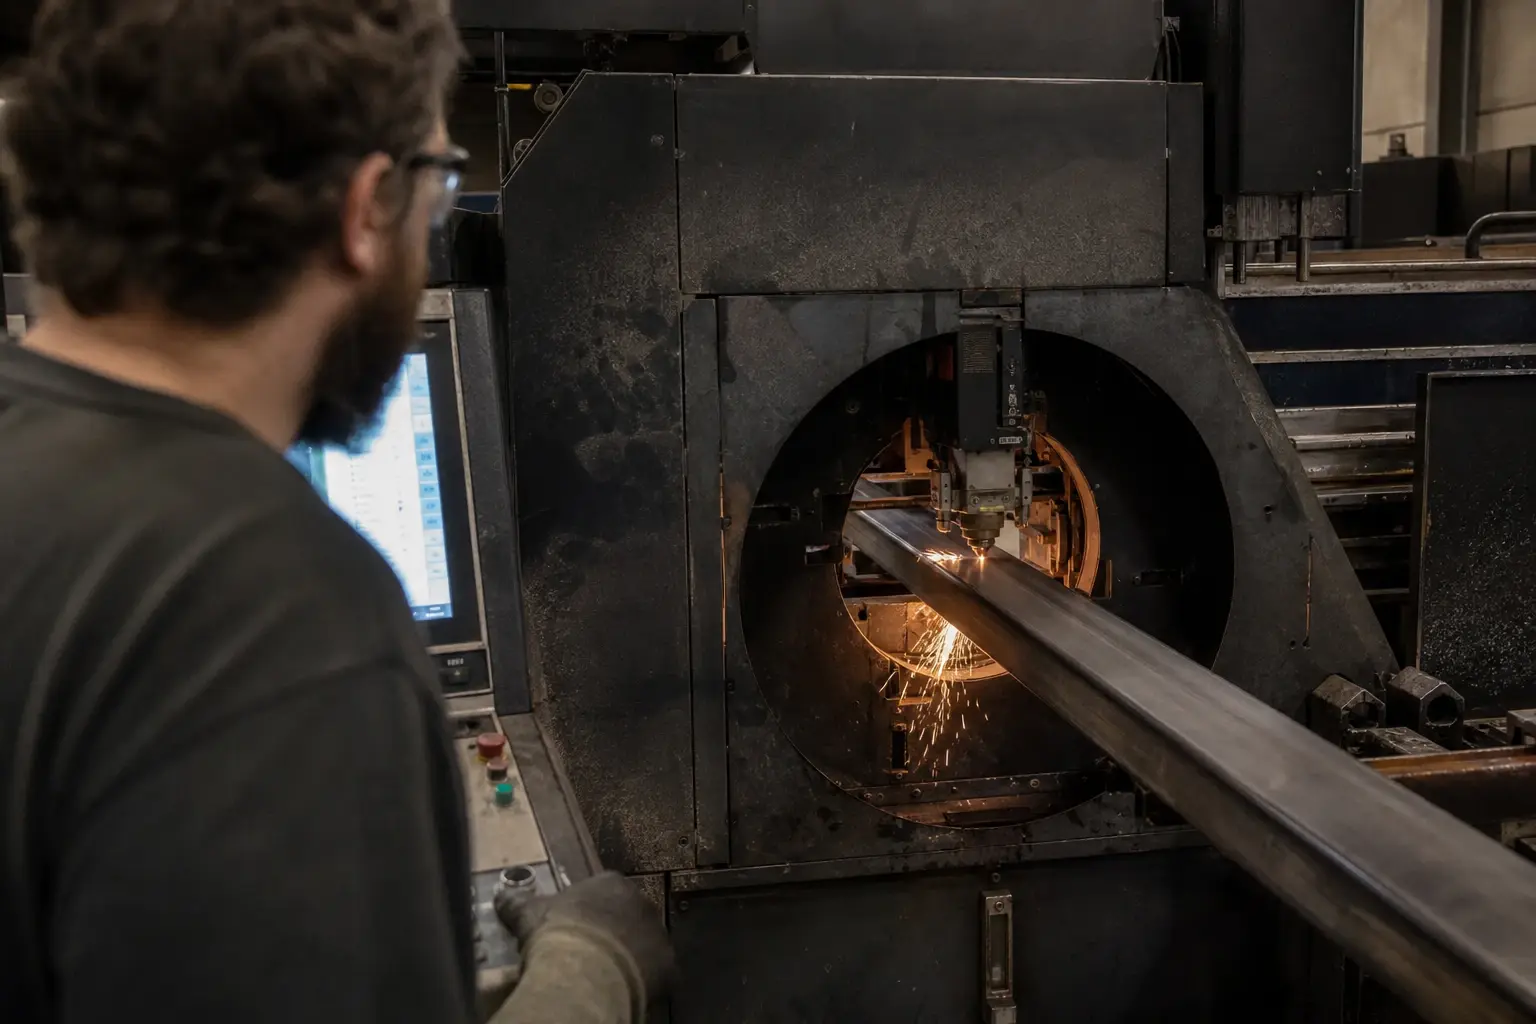
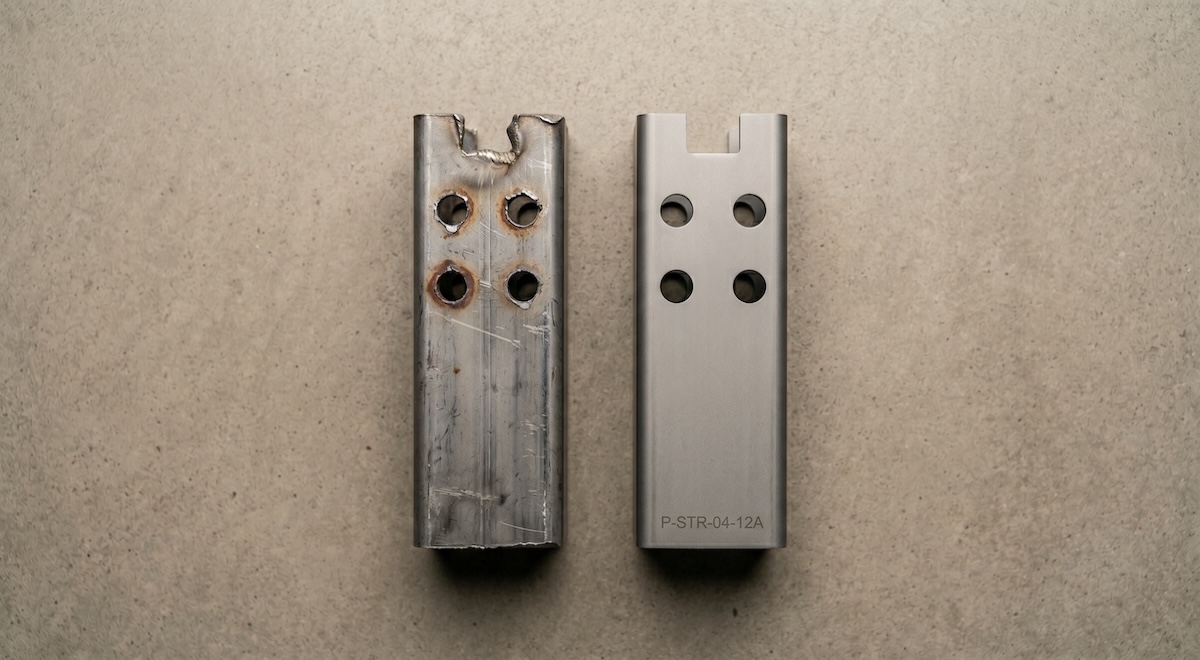
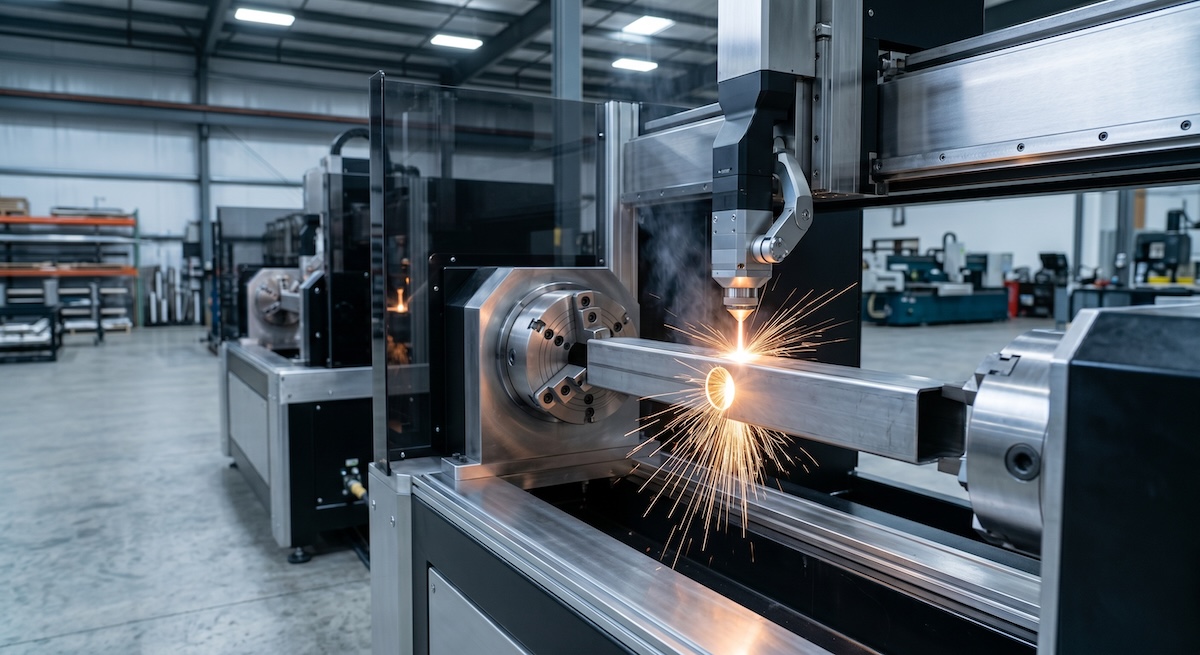
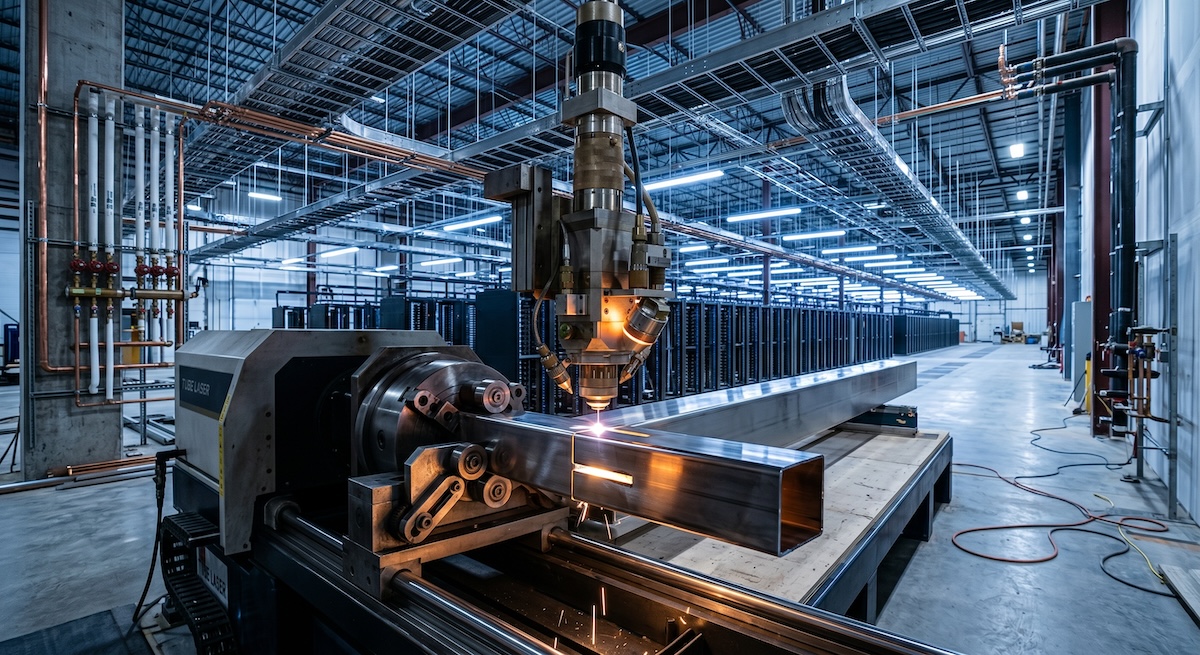
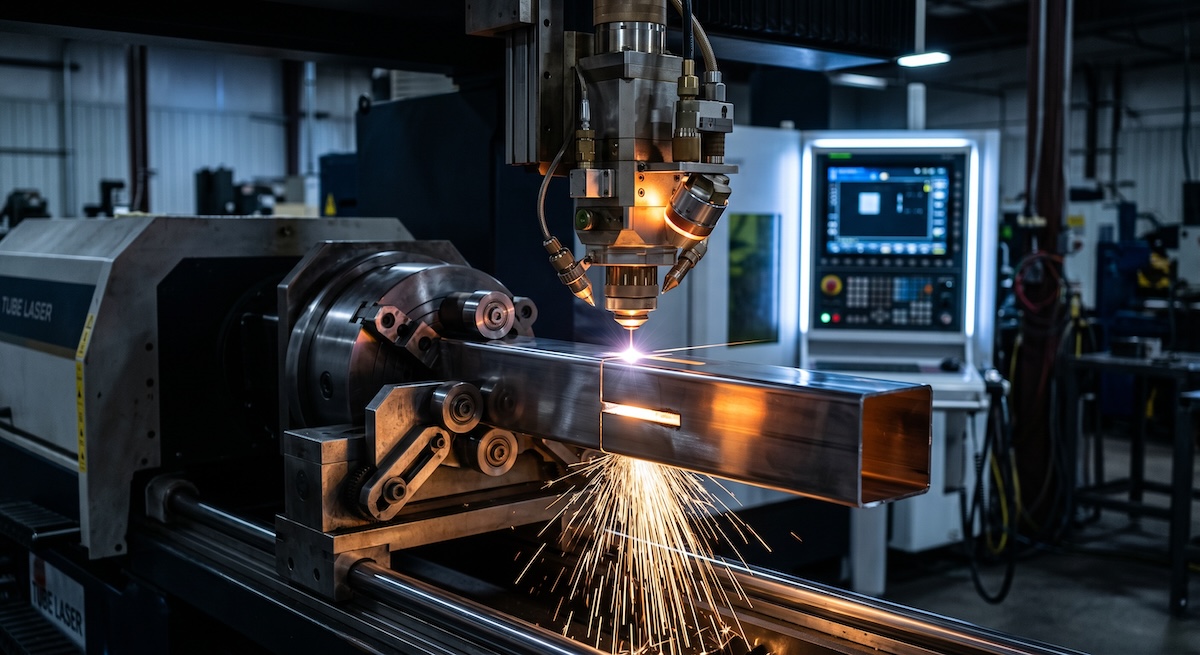
A saw-and-drill line splits the work across machines. A saw cuts the tube to length, a drill press or similar station adds holes, and other tools handle slots, notches and edge cleanup. A tube laser holds the tube in chucks and cuts the length, holes, slots and profiles with one beam, in one setup.
Published sources describe the same split. One tube lasering overview says laser machines can cut, drill and form tube in a single pass, while conventional methods often need follow-up drilling and finishing. A Trumpf page on tube lasers says laser tube cutting can save entire process steps.
Blueline runs LT7 tube lasers. Per its equipment list, these are 4kW, fully automatic machines that handle tube up to 6 inch square or round. Blueline also states it can process tube up to 13 inch diameter with 5-axis beveling capability.
How many steps does each route add to one part?
Count every time a person or a conveyor moves the tube to a new station. On a saw-and-drill route, each feature on the print can mean a new fixture and a new handling step. On a tube laser, most features come off the same setup.
Feature on the printSaw and drill routeTube laser routeCut to lengthSaw stationLaser, same setupAngled or mitered endSaw, reset to the angleLaser, same setupHolesDrill station and fixtureLaser, same setupSlots and notchesSeparate tooling or manual workLaser, same setupEdge cleanupOften a separate stepCan be reduced, depends on the partHandling between stationsOne move per stationFewer moves
The table is a starting point, not a promise. A part with only a square cut and no holes has one operation either way. A part with six features has six chances to go wrong on the older route.
What the sources say about steps
The same overview notes that traditional methods lose on drilling and finishing, which it calls time-consuming and labor-intensive. Another industry article says laser cutting handles complex contours, holes and cutouts in a single setup without tooling changes. Neither source gives a time saving figure, so this post does not either.
Where does saw and drill still make sense?
Saw and drill makes sense for plain square cuts, very simple parts and one-off jobs where tooling cost matters most. One source says conventional methods have the edge in the short term, because they are quicker to set up and cheaper. A cold saw also leaves a clean, burr-minimized cut and puts less heat into the material.
That last point matters. Laser cutting involves significant energy input, which can create a heat-affected zone near the cut. For parts where a plain saw cut is all the print needs, a saw is a fair choice.
If a part has holes, slots, coped ends or angled cuts, the argument shifts toward the laser. Our related guide on CNC tube cutting vs manual fabrication covers the manual end of that spectrum.
How do handling and stacked tolerances affect OEM parts?
Every time a tube is clamped again, the position of the next feature depends on that new clamp. Hole position, slot position and end angle each carry their own small error. When features come from different setups, those errors stack. A single setup keeps all features tied to one reference.
This is general shop-floor logic, not a measured result. The numbers that matter are the ones on your drawing and on your first-article inspection.
Blueline states tolerances of plus or minus 0.003 inch. According to Blueline, single-operation processing can reduce error rates by up to 70%. Treat both as the shop's own claims and confirm them on your part with a sample run.
Scale changes the math
Handling cost grows with volume. In 2025 Blueline processed 16 truckloads of stainless steel for an AI data center cooling project in Sacramento. At that scale, every avoided station is repeated thousands of times. For a closer look at high quantities, see the tube laser cutting for manufacturing OEMs service page.
What should OEM buyers send to compare both routes?
Send the drawing, the material and grade, the tube size and wall thickness, and the quantity. Add which features are critical and which are cosmetic. With those five items, a shop can say which operations the part needs and which route fits.
Our guide on how to get a tube laser fabrication quote for OEM projects walks through the same list in more detail. For slots, notches and holes specifically, see precision slotting, notching and hole cutting.
Frequently Asked Questions
Is a tube laser always faster than a saw?
No. For straight square cuts, a saw can be quicker to set up and cheaper to run. A tube laser tends to win when the part has several features, because those features come from one setup.
Can a tube laser replace drilling?
For many holes, yes. A tube laser can cut holes in the same setup as the length cut. Threaded holes still need a tapping step, so confirm with your fabricator which holes the laser can finish.
Does laser cutting leave a heat-affected zone?
Laser cutting adds heat near the cut edge, and a saw adds less. For most structural and OEM parts this is acceptable, but critical parts should be reviewed with the shop before cutting.
What does Blueline state about tolerances?
Blueline states tolerances of plus or minus 0.003 inch. Confirm the tolerance on your specific material, wall thickness and part before you rely on it.
What size tube can Blueline process?
According to Blueline, its LT7 tube lasers handle up to 6 inch square or round tube, and it can process tube up to 13 inch diameter with 5-axis beveling capability. See the tube laser cutting services page for current capabilities.
Get the Count Right Before You Pick the Machine
Pick the route after you count the operations on the print, not before. If the count is more than one or two, a tube laser deserves a quote. Blueline Industries in Chino, CA can review your drawing and tell you which route fits.
Get a Quote or call (951) 833-5597.