Quick Summary
- Tube laser cutting gives cleaner edges, smaller heat-affected zones and the ability to cut small slots and holes. Plasma is a fit for very thick wall.
- Sources set the thickness crossover at different points, roughly 16 mm to 30 mm, so confirm your wall with the shop.
- Plasma machines cost less to buy, but rough edges can add grinding before welding.
- Blueline in Chino, CA runs LT7 tube lasers and states tolerances of plus or minus 0.003 inch.
Tube laser vs plasma cutting comes down to wall thickness and feature detail. Laser wins on clean edges and small features in most tube work. Plasma earns its place on very thick wall where speed and machine cost matter more than edge finish.
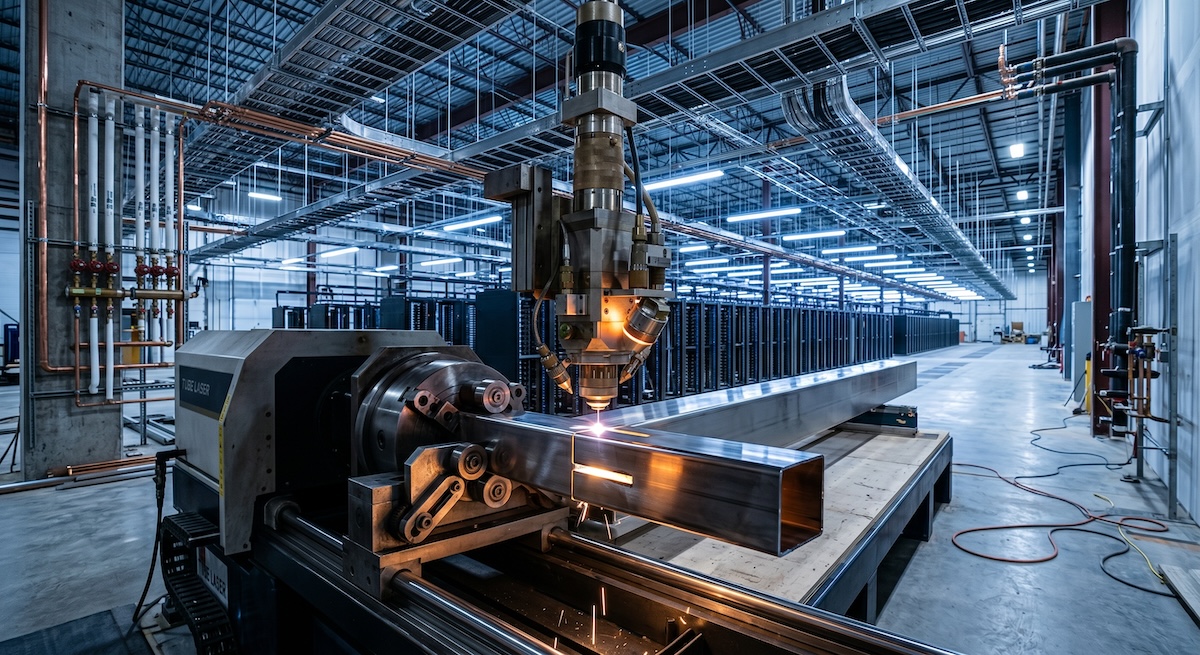
Blueline Industries does tube laser cutting from its Chino, CA facility for OEMs, contractors and fabricators. This post lays out how the two processes differ on tube and how to decide which fits your job.
How do tube laser and plasma cutting differ on tube?
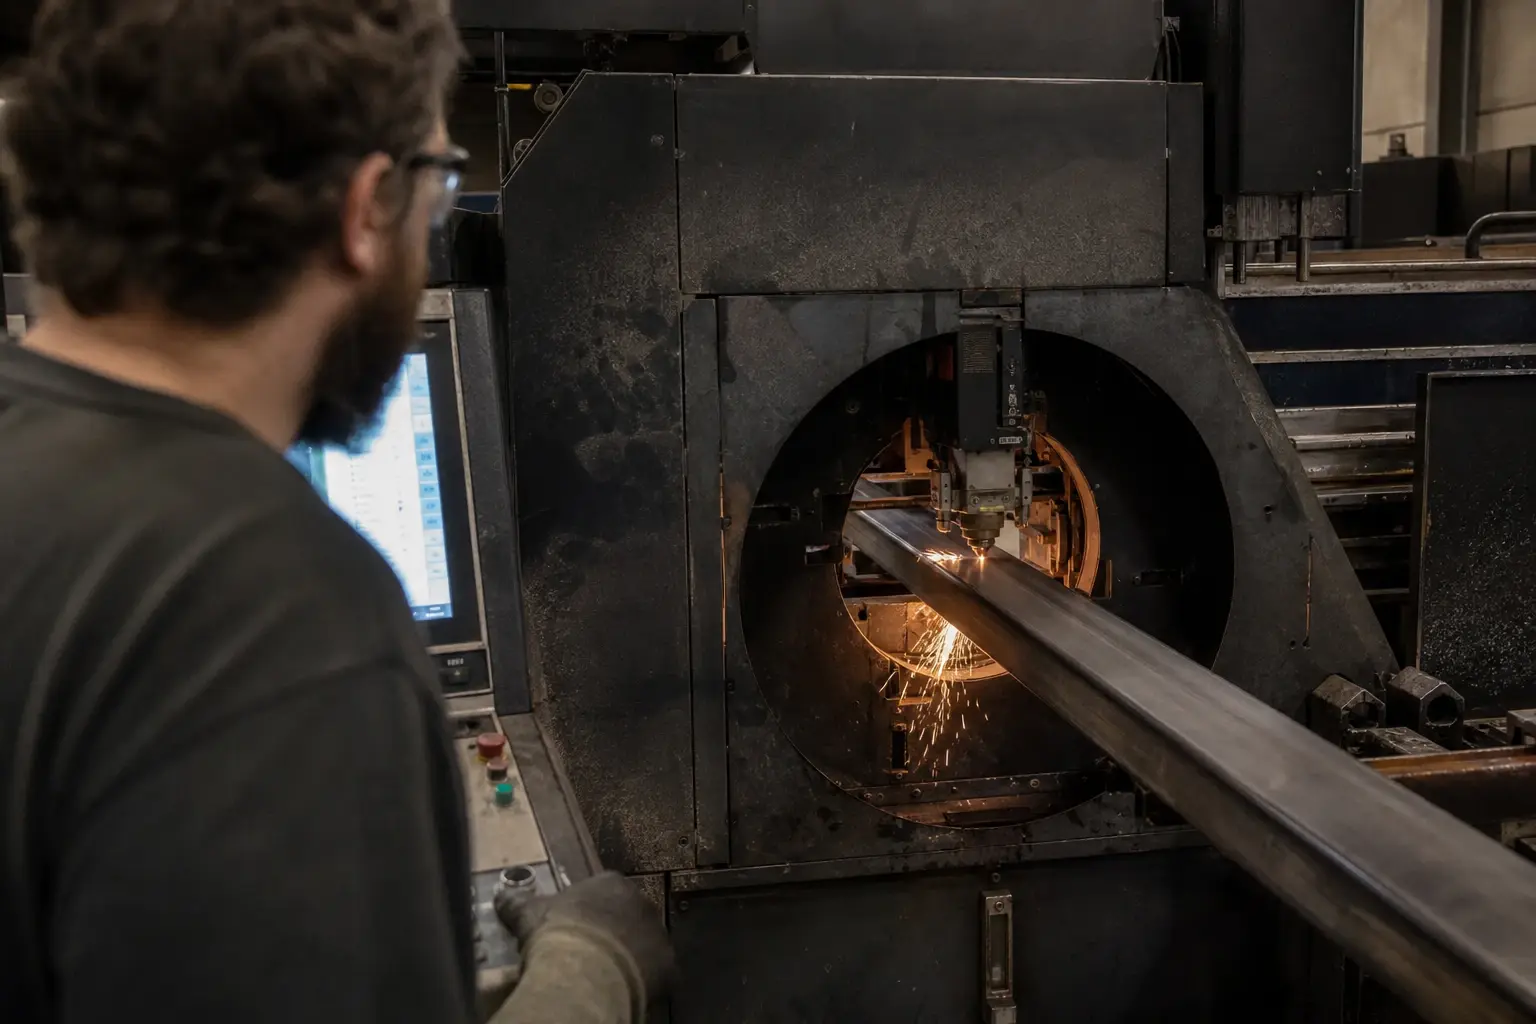
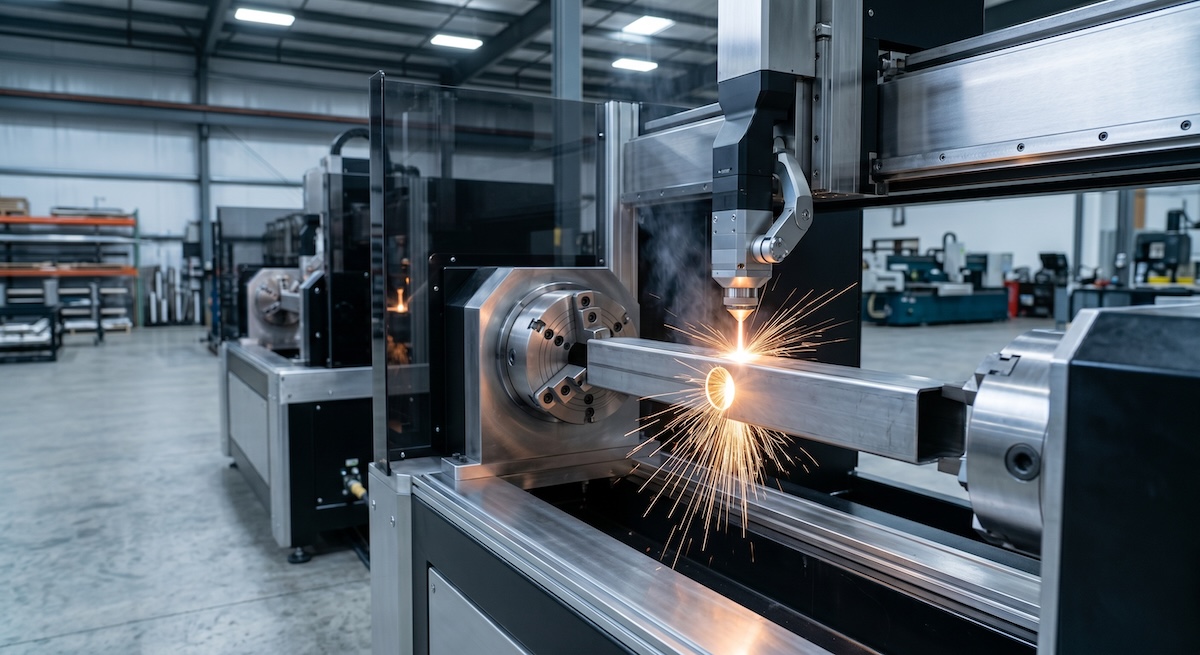
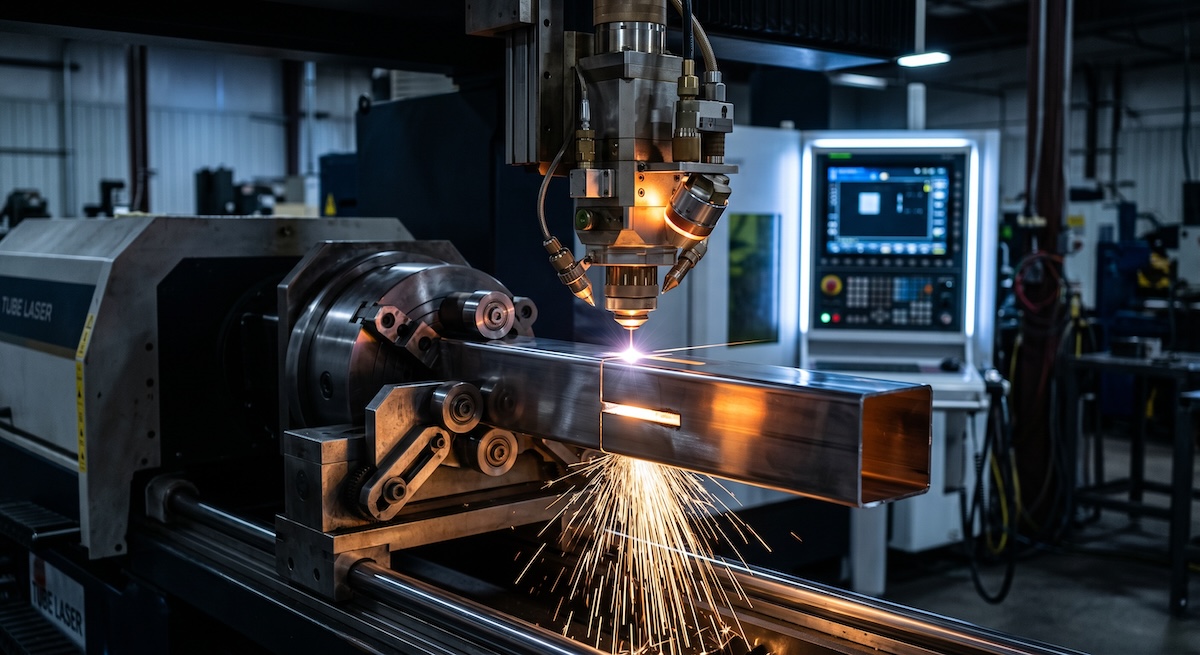
A tube laser uses a focused beam to cut tube, while plasma uses an electrically heated gas jet. Laser produces a narrower cut, a smaller heat-affected zone and cleaner edges. Plasma cuts thicker material and costs less to buy. BLM Group, which builds tube cutting machines, describes these trade-offs in its own comparison.
In its comparison of laser and plasma in tube cutting, BLM says the heat-affected zone is "much smaller in laser cutting." It also says the material removed by the cut is generally smaller with laser.
The heat-affected zone is the area next to the cut where heat changes the metal. A smaller one usually means less distortion and fewer surprises at the weld.
Which process gives cleaner edges and less rework?
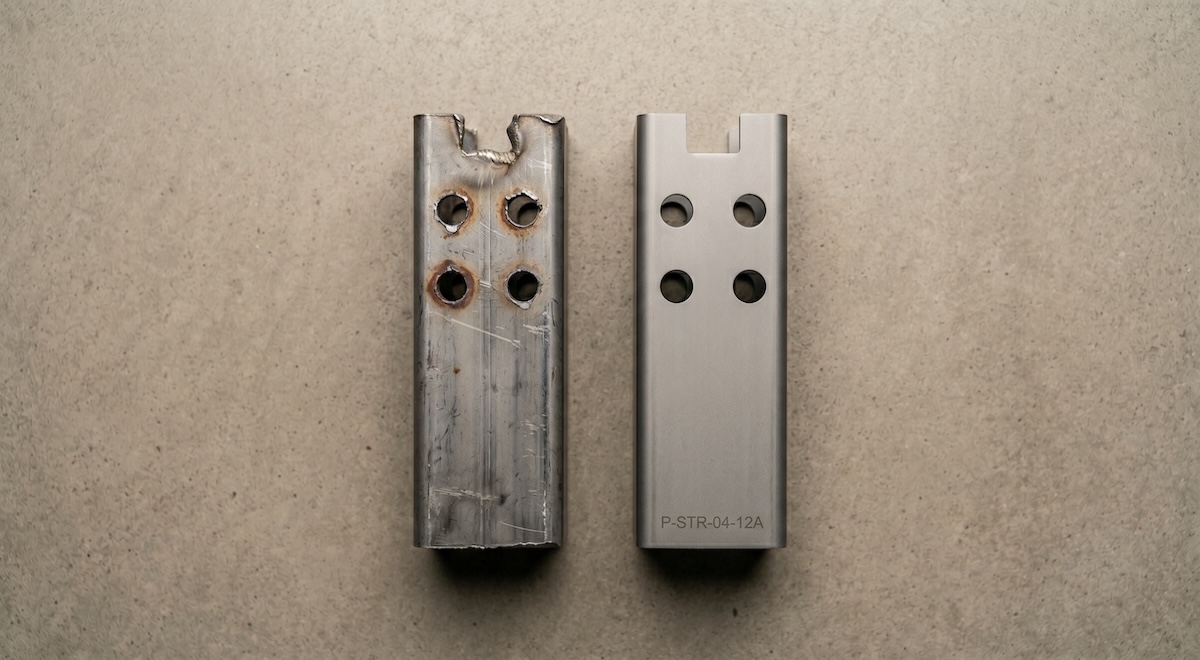
Laser gives cleaner edges and less rework in most tube jobs. BLM says laser-cut tubes are ready for the next welding phase with little to no need for extra edge preparation. It says plasma has a higher tendency to form burrs that need grinding or machining.
Rework is where the real cost hides. Every grinding pass adds labor and another chance to change a fit-critical dimension.
Blueline processed more than one million pounds of steel for the Coachella Sahara Stage in 2025. At that kind of volume, each extra finishing step multiplies across every part.
Small slots and holes
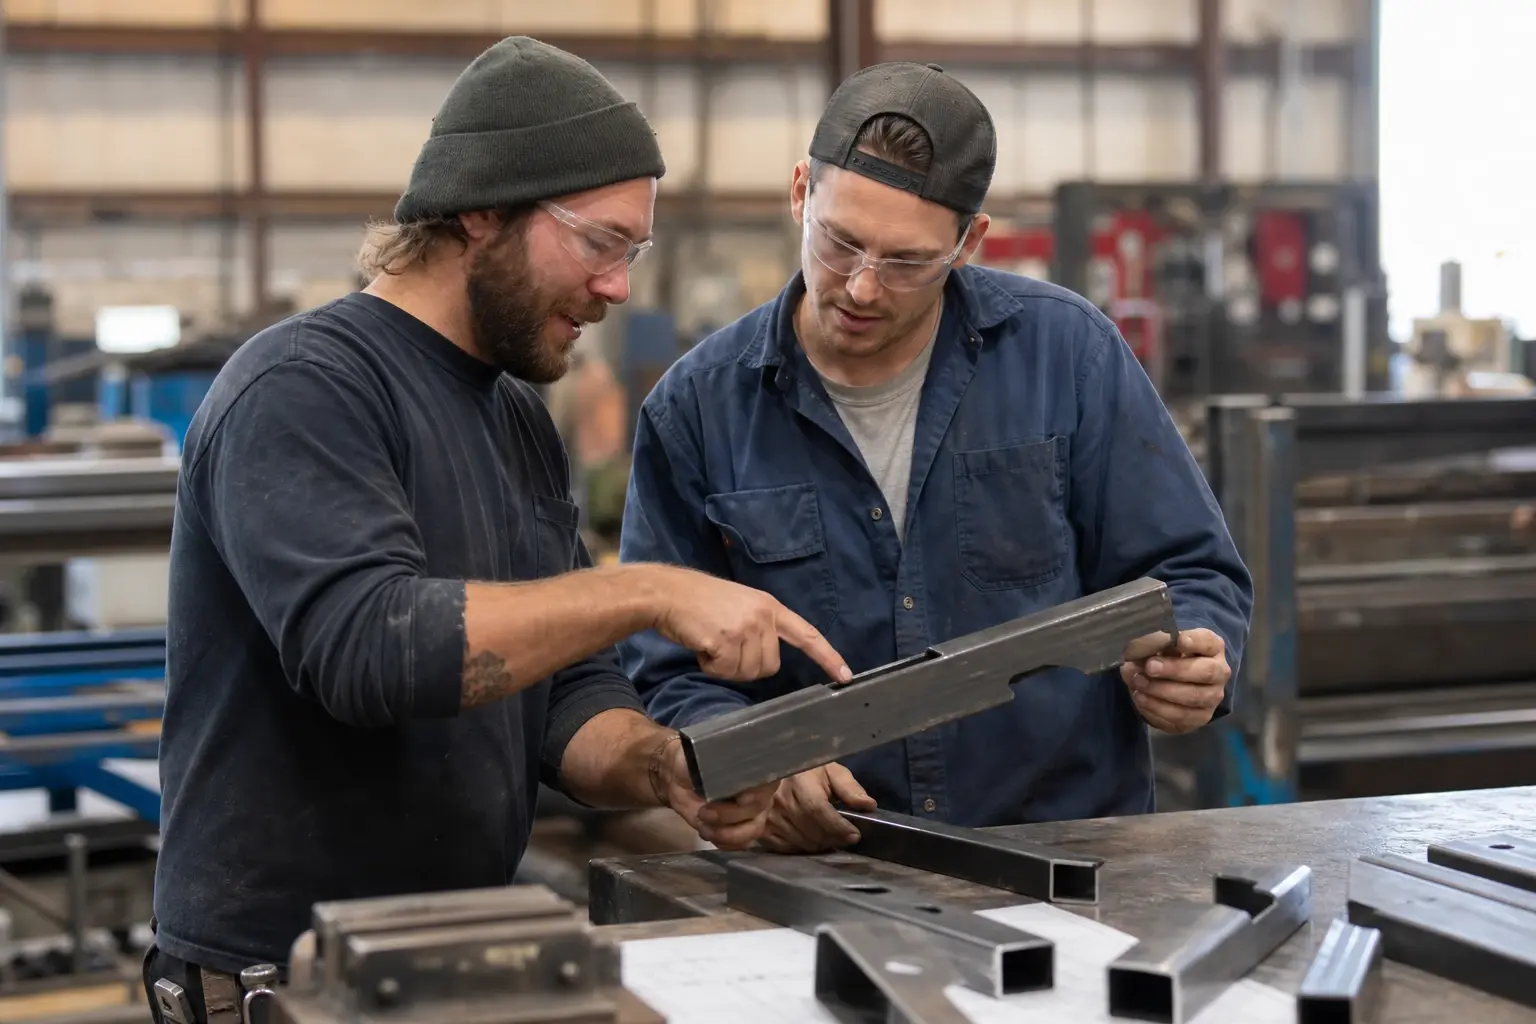
Feature size is another separator. BLM states that plasma cannot be used to cut holes or slots of small width, and that laser can cut holes with a diameter-to-thickness ratio of up to 0.5. If your tube needs tight slots, notches or hole patterns, laser is the practical choice.
Blueline's precision slotting, notching and hole cutting service covers those features.
When does plasma make more sense for tube?
Plasma makes sense on very thick wall and when machine budget is tight. Hypertherm, a plasma manufacturer, says plasma excels over fiber laser above 16 mm (5/8 inch) and that plasma machines typically cost 2 to 5 times less to buy. BLM recommends plasma for thickness from 30 mm to 80 mm.
Those sources come from companies that sell plasma or tube cutting equipment. Treat the thresholds as guidance, not a rule. Wall thickness, material and the features you need decide the answer for your part.
Plasma is also generally not considered for tube under 25 mm (1 inch) in diameter, according to BLM. Small tube points you toward laser.
Tube laser vs plasma: side-by-side
| Factor | Tube laser | Plasma |
|---|---|---|
| Edge quality | Cleaner edges, little edge prep per BLM | More burrs, grinding often needed per BLM |
| Heat-affected zone | Much smaller per BLM | Larger on average per BLM |
| Small holes and slots | Yes, hole diameter to thickness ratio up to 0.5 per BLM | Not suited to small-width holes or slots per BLM |
| Small tube diameter | Handles a wide range of sections | Generally not considered under 25 mm (1 inch) per BLM |
| Thick wall | Strong up to about 20 mm (1 inch) per BLM | Recommended over 30 mm (1 1/8 inch) per BLM |
| Machine purchase cost | Higher | Typically 2 to 5 times less per Hypertherm |
How do you choose between them for your tube job?
Start with wall thickness, then check features, downstream welding and volume. If the wall is well under about 20 mm and the part has slots, notches or holes, choose laser. If the wall is very thick and the cut is plain, plasma deserves a look.
A quick checklist
- What is the tube size and wall thickness?
- Does the part need small slots, notches or hole patterns?
- Will the part be welded, and does the edge need to be weld-ready?
- How many parts do you need, and will they repeat?
- Do you need beveled ends or other angled cuts?
On equipment, Blueline's LT7 tube lasers are 4kW machines that handle up to 6 inch square or round tube and run fully automatic. The shop also states it can process tube up to 13 inch diameter with 5-axis beveling capability. Blueline states tolerances of plus or minus 0.003 inch. See steel tube laser cutting for the shop's steel work, or read Tube Laser Cutting Explained for the basics.
What should you send when you ask for a tube cutting quote?
Send a dimensioned drawing or 3D model, tube shape and size, wall thickness, material grade, quantity and any bevel or finish needs. Mark the features that control fit. With that information, the shop can tell you quickly whether laser suits the job.
Two extra details help more than people expect. First, say how the part will be welded, because that decides how clean the edge must be. Second, say whether the part will repeat, because repeat work justifies more programming time up front.
If the design is not final, ask for a short run first. A small batch shows you how the cut edges, slots and holes behave in your assembly before you commit to volume. That is cheaper than finding a fit problem after a full release.
Frequently asked questions
Can a tube laser cut stainless steel?
Yes. BLM says laser can cut any kind of metal, including steel, stainless steel, copper and aluminum alloys. Blueline states its programs and material handling are tuned for sustained stainless production.
Is plasma cheaper than laser for tube?
The machine costs less. Hypertherm says plasma machines typically cost 2 to 5 times less than fiber laser systems. Part cost depends on rework, edge prep and features, so compare finished parts, not machine prices.
Does laser cutting leave burrs?
BLM says laser edges are cleaner and usually need little edge preparation before welding. Plasma has a higher tendency to form burrs. Results still vary with material and settings.
What tolerance can Blueline hold on tube parts?
Blueline states tolerances of plus or minus 0.003 inch. Send your drawing and critical dimensions so the shop can confirm what applies to your part.
Can a tube laser cut beveled ends?
Blueline states it can process tube with 5-axis beveling capability. Tell the shop the bevel angle and where it applies when you request a quote.
Send your tube job for a laser cutting quote
Pick the process by wall thickness and feature detail, then confirm with the shop that will cut it. Blueline reviews tube jobs from Chino, CA.
Get a Quote or call (951) 833-5597.