Quick Summary
- A complete spec package, sent before the first cut, is the fastest way to a clean aerospace tube part.
- Fiber lasers leave a small heat-affected zone, but you should still flag any edge that is sensitive to heat.
- Self-fixturing slots and single-piece designs cut handling and assembly error in prototypes.
- Blueline Industries in Chino, CA states a tolerance of plus or minus 0.003 inch and processes tube in a single operation.
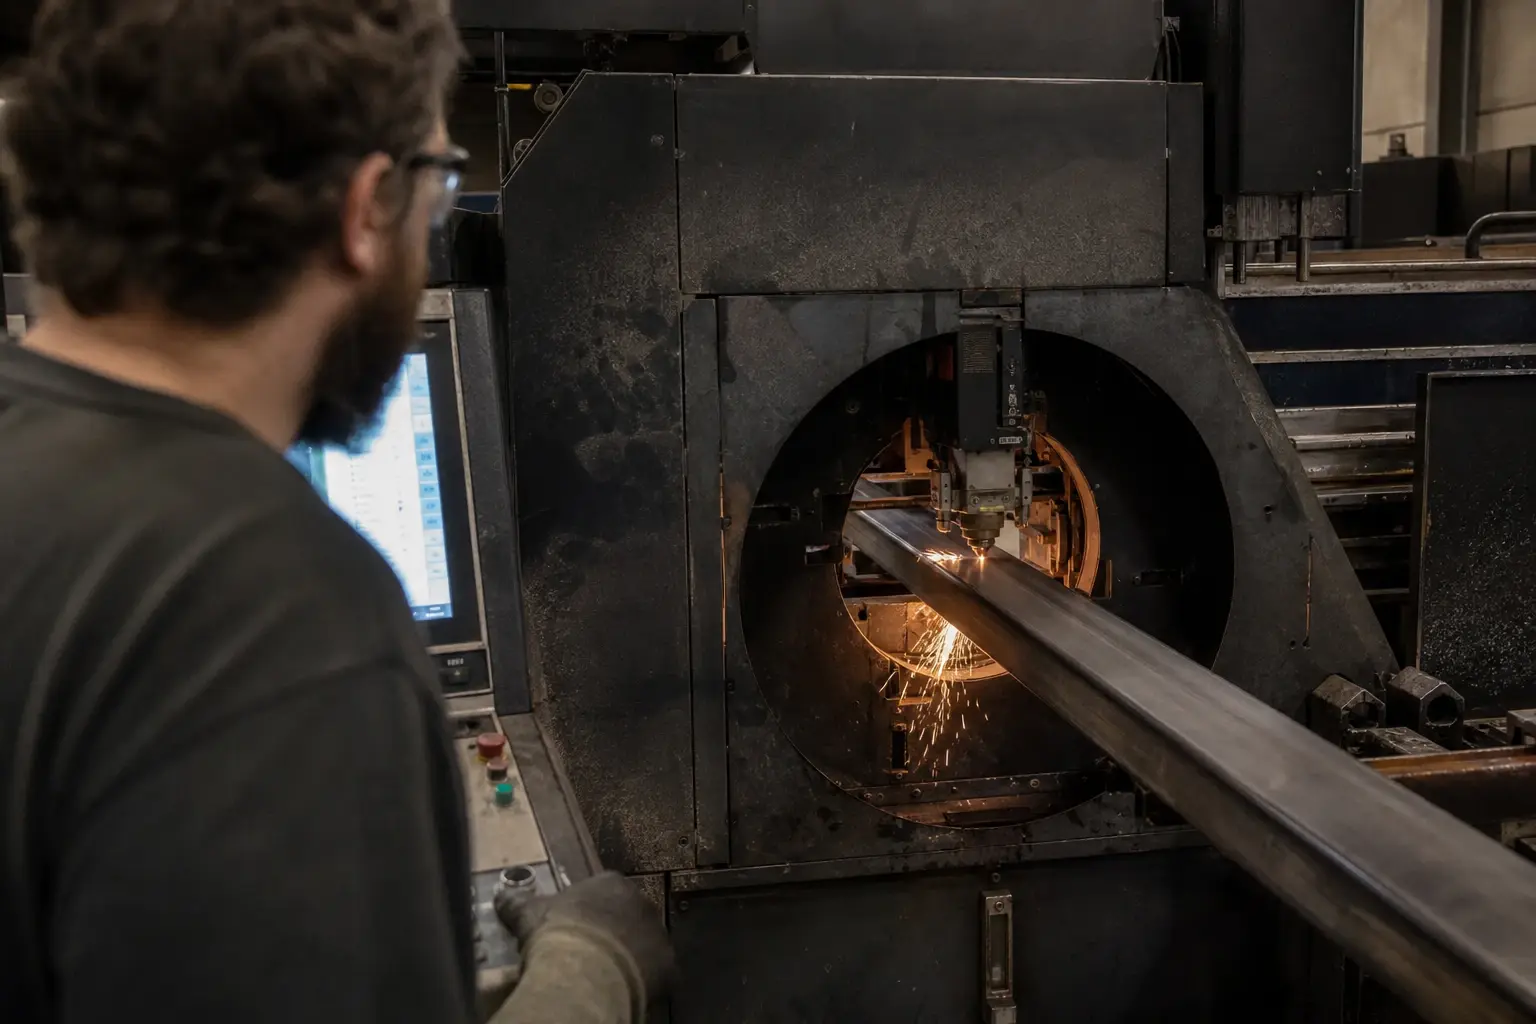
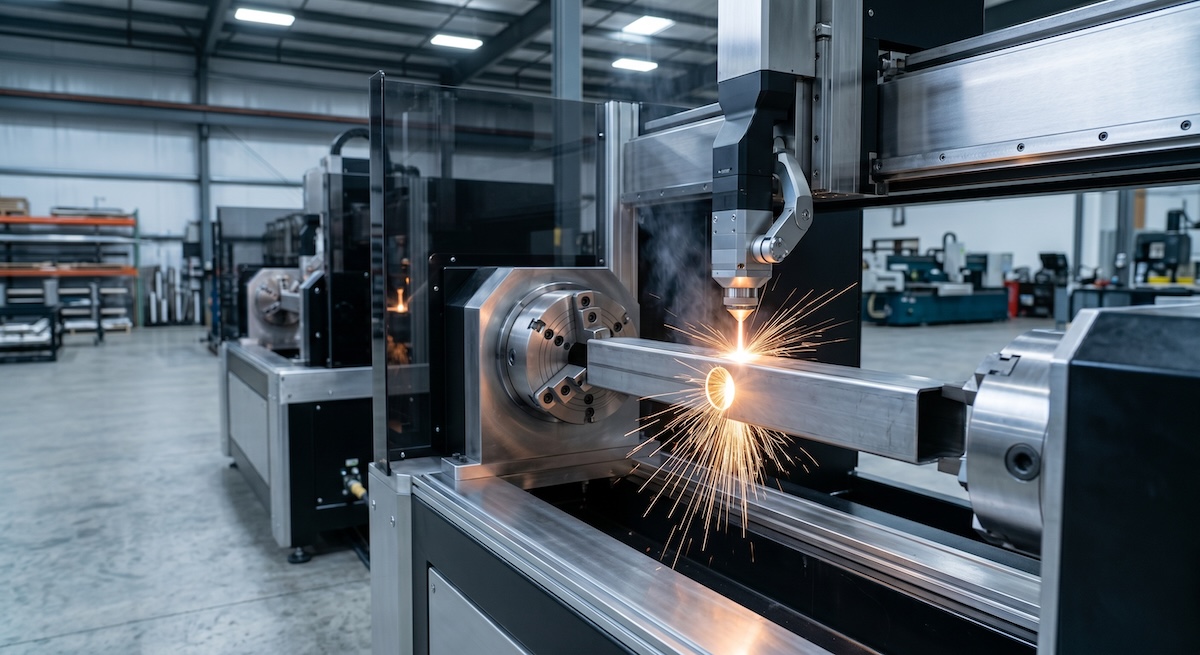
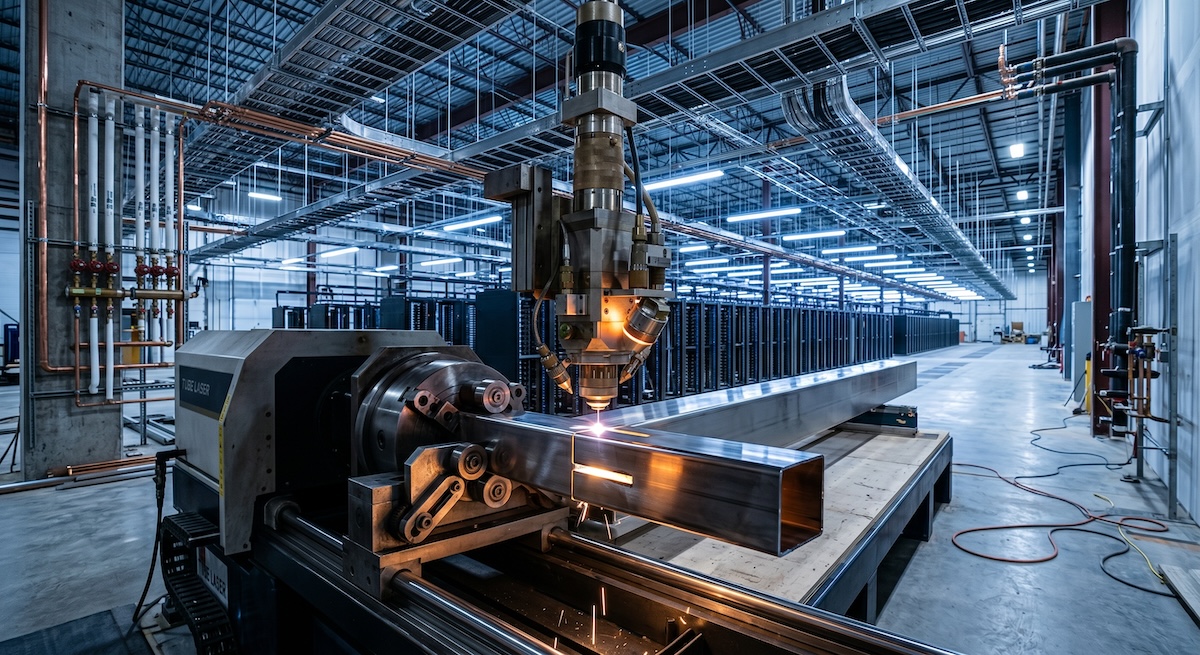
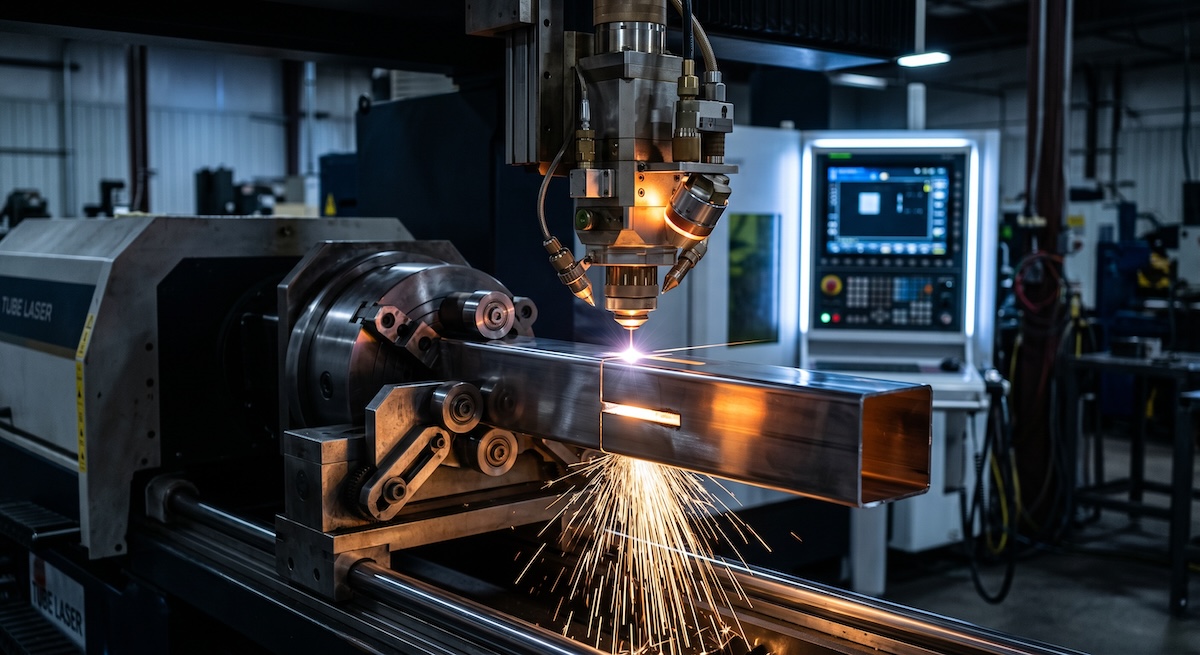
Aerospace tube laser cutting works best when engineers hand the shop a complete spec package before the first cut. Blueline Industries, a tube laser cutting shop in Chino, CA, cuts tube and structural profiles in a single operation, so slots, notches and holes come off one machine. This post covers what belongs in that package, how heat affects a cut part, and how to design prototypes that cut cleanly.
One note up front. Whether a given aerospace program fits depends on its material, documentation and approval requirements. Raise those early, and Blueline can tell you plainly whether the job is a match.
Is tube laser cutting a good fit for aerospace tube parts?
Tube laser cutting suits aerospace-style tube parts that need repeatable slots, notches and holes from one setup. Fiber lasers also leave a small heat-affected zone compared with older CO2 machines. Fit still depends on your material, documentation and approval requirements, so confirm those with the shop before you finalize a design.
Advanced Manufacturing reports that five-axis laser cells deliver consistent repeatability while minimizing scrap. The same article says fiber lasers generate "extremely minimal" heat-affected zone, while older CO2 lasers could leave perimeters brittle and more prone to fractures.
Blueline runs LT7 tube lasers, which the company states are fully automatic and handle square and round tube up to 6 inches. Blueline also states it processes tube up to 13 inches in diameter with 5-axis beveling capability. Those numbers are worth checking against your part envelope on day one.
What should an aerospace tube laser cutting spec package include?
Send a drawing and a 3D model, the tube material and wall thickness, quantity, critical tolerances, and any finish or documentation needs. Add the revision level and mark which features matter most. A complete package lets the shop quote accurately and flags problems before cutting starts instead of after parts arrive.
| Spec item | Why it matters |
|---|---|
| Drawing and 3D model | The model drives the cut path. The drawing carries tolerances and notes. |
| Material and wall thickness | Both change cut settings, edge condition and what the shop can run. |
| Tube shape and size | Square, round and rectangular tube load and cut differently. |
| Critical features | Marking the features that matter keeps tight tolerances where you need them. |
| Quantity and release plan | One prototype, a short run and a repeat order are quoted differently. |
| Finish and documentation | Edge finish, inspection reports and paperwork should be settled before quoting. |
| Revision level | The shop cuts the right version and you can trace any change. |
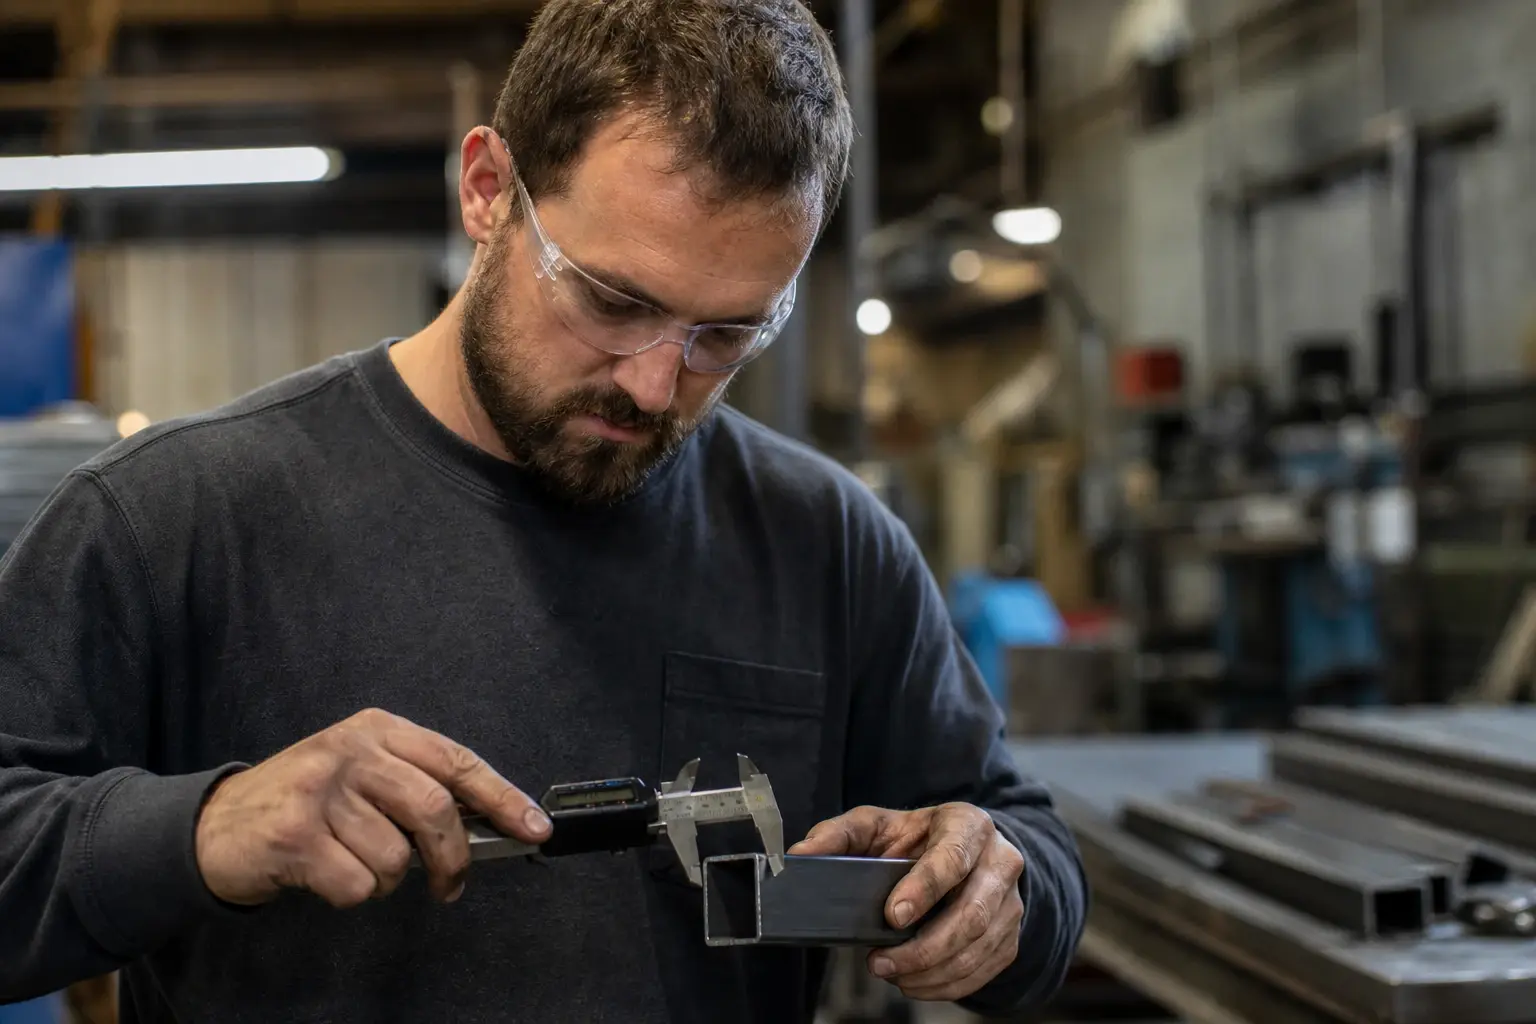
Blueline states tolerances of plus or minus 0.003 inch. Tell the shop which features truly need that level and which can be looser. Tolerances applied everywhere add inspection effort without adding value.
If you have not sent a request like this before, the guide to getting a tube laser fabrication quote walks through the same basics.
How does heat affect aerospace tube parts after laser cutting?
Laser cutting creates a heat-affected zone, the band between melted metal and unaffected base metal that undergoes structural change. According to The Fabricator, laser cutting produces the smallest such zone of the thermal cutting methods. Its size depends on heat applied, exposure time and area affected.
The same article notes that removing the zone completely means machining it away. That lowers material yield and adds labor and machine time. For a part with a heat-sensitive edge, plan for that cost in the design stage rather than discovering it at inspection.
Questions to settle about cut edges
- Which edges are structural, and which are only locating features?
- Does any edge get welded, bent or machined after cutting?
- Is there a finish or inspection requirement on the cut face?
Answers to these three questions let the shop set expectations and let you decide whether a secondary step belongs in the plan. Blueline offers precision tube fabrication that includes press brake bending, so bending and cutting can be planned together.
How do you design aerospace tube prototypes for the laser?
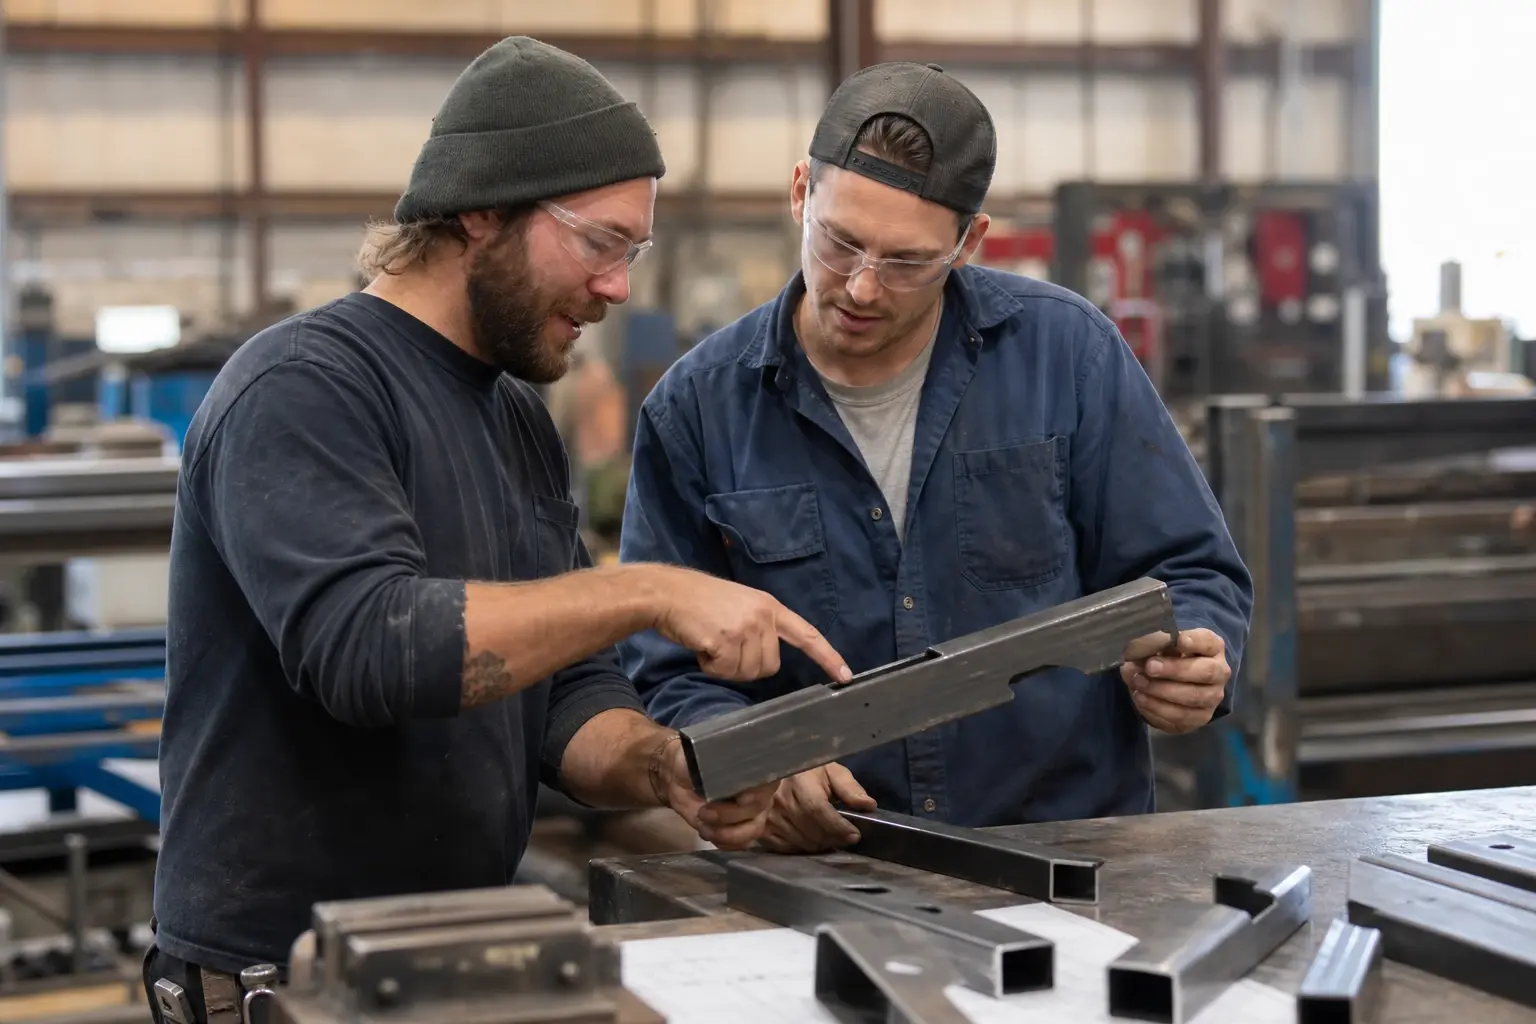
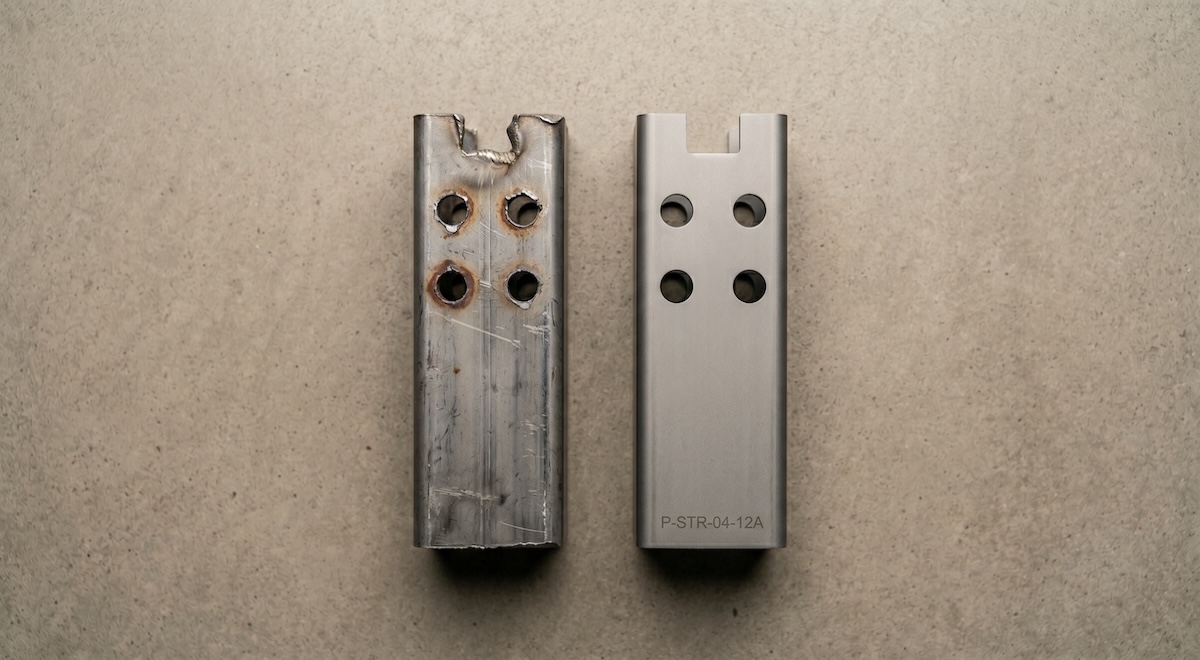
Cut features from a single piece where you can, and use self-fixturing hook-and-slot designs so parts locate themselves during assembly. Fewer pieces mean less handling and fewer chances for error. Share the model early so the shop can suggest changes before you commit to a design.
The Fabricator recommends these same ideas: self-fixturing hook-and-slot designs reduce cost and assembly errors, and cutting one component from one piece rather than four simplifies fixturing. It adds that a laser can cut a tube to length and create any shape of end cut or wall opening, including a radius corner on square or rectangular tube.
That freedom is useful in prototyping, where design changes arrive fast. Blueline's custom tube prototyping and short-run fabrication service is built for that stage. A cut-and-fit loop on real tube tells you more than another round of drawings.
What does stainless tube processing look like at scale?
At scale, stainless tube processing is mostly about keeping every part consistent across a large order. Blueline's verified example is an AI data center cooling project in Sacramento, completed in 2025, which involved 16 truckloads of stainless steel. It is a different industry from aerospace, but the stainless tube work is the same discipline.
Blueline states that single-operation processing can reduce error rates by up to 70%, because fewer machining steps mean fewer handoffs. For aerospace-style parts, the practical takeaway is simple. Ask how many separate operations your part needs, and whether any can be folded into the laser cut. See the stainless steel tube processing page for what Blueline lists.
Frequently Asked Questions
What materials does Blueline cut for aerospace-style parts?
Blueline lists steel and stainless steel tube processing as core services. Industry sources say lasers can cut other alloys, but whether a specific shop runs a specific alloy has to be confirmed. Send your material callout with the quote request.
Can tube laser cutting hold aerospace tolerances?
Blueline states tolerances of plus or minus 0.003 inch. Your drawing decides what is required. Send the drawing so the shop can compare your callouts to what it can hold and tell you where a feature needs a closer look.
Do I need to send a 3D model?
A 3D model is the best starting point because it drives the cut path. Send the drawing too, since it carries the tolerances, notes and revision level. Together they remove most of the guesswork.
Does Blueline build prototypes before production?
Yes. Custom tube prototyping and short-run fabrication is one of Blueline's core services. A prototype run is a low-risk way to check fit before you release a larger order.
Where is Blueline, and can it ship parts?
Blueline operates from one facility in Chino, CA 91710. The company ships to buyers in its service area, including Los Angeles, San Diego, San Jose, San Francisco, Las Vegas, Tucson, Salt Lake City, Portland and Seattle. See the service area page for details.
Next step
A good aerospace tube job starts with a complete package and an honest conversation about requirements. Send your drawing, model, material and quantity, and flag any approval or documentation needs up front.
Ready to talk through your part? Get a Quote or call (951) 833-5597. You can also review Blueline's tube laser cutting services.